Introduction
In modern manufacturing, achieving the “perfect blend” is as much a precise science as it is a critical operational milestone. In sectors like food, pharmaceuticals, and nutraceuticals, the homogeneity of powders and granules is the primary driver of product stability and regulatory compliance. Consequently, the mixing technology integrated into your production line is more than just hardware; it is the cornerstone of quality assurance and operational throughput.
Among the diverse array of industrial mixing solutions, the ribbon blender remains the gold standard, prized for its versatile performance and proven reliability. Whether you are designing a new facility or upgrading a legacy system, understanding the nuances of ribbon blender technology is essential. The right choice doesn’t just improve mixing times, it ensures product consistency, optimizes overhead, and safeguards the continuity of your operations.
This guide offers a practical, deep-dive analysis into the performance metrics and selection criteria of ribbon blenders, empowering you to make data-driven decisions tailored to your specific production demands.
What is A Ribbon Mixer?
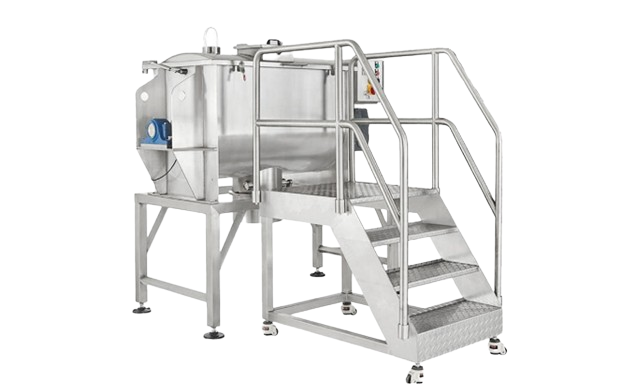
The ribbon blender features a horizontal U-shaped trough housing a dual-ribbon agitator driven by a central shaft. This configuration utilizes an inner and outer ribbon designed to rotate in opposing directions. Specifically engineered for high-homogeneity blending, this system excels at processing dry powders, granules, and mid-viscosity semi-solids in industries where strict uniformity is paramount.
Unlike drum mixers that rely on gravity-fed diffusion, the ribbon blender employs a composite mechanism of forced convection and shear. As the ribbons rotate, the outer flighting draws material from the ends of the vessel toward the center, while the inner flighting pushes material from the center outward. This countercurrent flow creates a high-intensity, three-dimensional “vortex” effect. This ensures not only the rapid macroscopic blending of bulk components but also the microscopic dispersion of trace additives—effectively eliminating material stratification and agglomeration.
Ribbon blenders have established themselves as the industry standard across the food, pharmaceutical, chemical, and new energy sectors, primarily due to their superior performance across three key dimensions:
Rapid Cycles & Precision Homogeneity
Most standard materials achieve a “perfect blend” within a 3–15 minute cycle. With a Coefficient of Variation (CV) consistently maintained below 5%, these mixers meet even the most stringent quality standards. This high turnover rate boosts overall plant throughput, making it an ideal choice for both batch and continuous production lines.
Versatile Material Compatibility
These systems are exceptionally adaptable, capable of handling bulk density ratios as wide as 1:3. Whether you are processing lightweight seasonings (below 0.3 g/cm³) or dense mineral and battery cathode materials (above 1.5 g/cm³), the ribbon configuration, RPM, and fill levels can be customized to suit your needs—even for fragile particles or semi-viscous substances.
Optimized ROI & Operational Reliability
Compared to high-shear or fluidized bed systems, ribbon blenders offer a significantly lower Total Cost of Ownership (TCO). The streamlined mechanical design—free of complex pneumatic systems or high-speed rotors—minimizes failure points. This results in lower energy consumption, simplified maintenance, and easier wash-downs, providing the perfect balance of performance and reliability.
Enhanced Versatility: Modern units can be further customized with heating/cooling jackets, liquid spray manifolds, and vacuum or inert gas purging, transforming a standard mixer into a multi-functional reactor for drying, coating, or chemical processing.
Ready to achieve the “perfect blend” for your production? Explore the SED-DH Series Industrial Ribbon Blender from SED Pharma—engineered for high homogeneity and precision across food and pharmaceutical sectors.
Configurations of Ribbon Blenders in Core Industries
The design of a ribbon blender is never “one-size-fits-all.” To be truly effective, the equipment’s configuration must be precision-engineered to align with specific process workflows, stringent regulatory mandates, and the unique physical properties of the materials involved. Across various sectors, what begins as a “standard” machine is transformed into a specialized, high-performance solution through targeted functional upgrades and compliant design features.
The following sections explore how ribbon blenders are customized to meet the rigorous demands of four key industries: Pharmaceuticals, Food & Beverage, Chemicals & New Energy, and Nutraceuticals.
Pharmaceutical Industry: GMP-Compliant Sanitary Design
In the pharmaceutical sector, ribbon blender engineering is governed by strict Good Manufacturing Practice (GMP) standards. Every design element must prioritize product purity, cross-contamination prevention, and full process traceability.
1. Materials and Surface Integrity
To meet stringent FDA and EMA requirements for direct-contact equipment, all wetted parts are typically fabricated from 316L stainless steel. Surfaces undergo high-precision mechanical or electrolytic polishing to achieve a finish of Ra ≤ 0.4μm. This ultra-smooth texture eliminates “dead zones,” prevents material adhesion, and ensures maximum corrosion resistance during aggressive cleaning cycles.
2. Advanced Sealing and Contamination Control
To safeguard batch integrity, these blenders utilize sanitary mechanical seals and a fully isolated drive system, effectively eliminating the risk of lubricant migration into the product chamber. Inlet and outlet ports are fitted with quick-release sanitary clamps or high-performance butterfly valves. All interfaces comply with international standards, allowing for seamless, closed-loop integration with upstream and downstream processing equipment.
3. Cleaning and Sterilization Validation (CIP/SIP)
The equipment is engineered to support automated Cleaning-in-Place (CIP) and Sterilization-in-Place (SIP) protocols. Integrated features include:
- 360° Rotating Spray Balls: Ensuring full coverage of the interior vessel.
- Dedicated Validation & Sampling Ports: Allowing for aseptic material sampling and rinse-water testing to ensure the cleaning process is both verifiable and repeatable.
4. Comprehensive Documentation and Lifecycle Support
To streamline the regulatory approval process, manufacturers provide a robust Validation Support Package. This documentation is essential for DQ/IQ/OQ/PQ (Design, Installation, Operational, and Performance Qualification) and typically includes:
- Material Traceability Certificates (MTRs)
- Surface Finish and Roughness Reports
- Weld Map and Inspection Records (NDE/NDT)
- FAT/SAT (Factory/Site Acceptance Testing) protocols
Food Industry: Engineering for Food Safety & Operational Hygiene
In food processing, ribbon blenders must balance high-throughput performance with uncompromising sanitary standards. The design focuses on mitigating microbial risks and streamlining the changeover process.
1. Certified Food-Grade Materials
All wetted components are fabricated from food-grade 304 or 316 stainless steel, with configurations available to meet NSF, 3-A, or EHEDG sanitary standards. To ensure chemical compatibility and safety, all non-metallic seals and gaskets are manufactured from FDA-approved elastomers, such as Silicone, EPDM, or PTFE.
2. Hygienic Structural Integrity
To eliminate potential “harborage points” for microbial growth, the blender utilizes large-radius internal sweeps (coved corners) and a bolt-free mixing shaft design. This ensures that no material residue is trapped in crevices. The discharge assembly typically features a sanitary butterfly or ball valve, engineered for tool-free disassembly to facilitate rapid deep-cleaning.
3. Cross-Contamination & Changeover Optimization
For facilities handling diverse product lines—such as seasonings, allergens, or health foods—we offer modular mixing components and dedicated hopper systems to accelerate product changeovers. For specialized applications involving acidic ingredients or high-fat content, surface treatments such as passivation or non-stick PTFE (Teflon) coatings are available to prevent material buildup and simplify wash-downs.
4. Process Intensification & Integration
To streamline the production chain, modern food-grade blenders are often equipped for multi-stage processing:
- Precision Liquid Injection: High-accuracy spray manifolds allow for the uniform addition of flavorings, oils, or fortificants during the cycle.
- Thermal Management: Integrated heating or cooling jackets enable simultaneous mixing and temperature control (e.g., for wetting or tempering), significantly reducing total processing time and equipment footprint.
Nutraceuticals & Medical Foods: Agile Production and Full-Chain Traceability
The nutraceutical and medical food sectors are characterized by diverse formulations, smaller batch runs, and rigorous regulatory oversight. To meet these challenges, ribbon blenders must offer enhanced operational flexibility alongside robust data integrity.
1. Intelligent Recipe Management
To accommodate a wide array of formulations, equipment can be integrated with an advanced automated control system. This allows for the storage of hundreds of discrete process profiles—including agitator speed, cycle times, temperature setpoints, and liquid injection volumes. This “one-touch” setup ensures seamless product changeovers and significantly reduces the risk of human error in complex production environments.
2. High-Precision Micro-Ingredient Dispersion
The uniform distribution of high-value active ingredients, such as vitamins, enzymes, and probiotics, is critical. We offer integrated micro-feeding systems with dosing accuracies of up to ±0.1%. When paired with a liquid spray dispersion manifold, these systems ensure that trace components are perfectly homogenized throughout the bulk carrier, preventing hotspots or under-dosing.
3. Data Integrity and Electronic Records
In alignment with FDA 21 CFR Part 11, our systems are engineered to support the highest standards of digital accountability. Key features include:
- Audit Trails: Comprehensive logging of all operator actions and setpoint changes.
- Parameter Trending: Real-time storage of process curves (temperature, torque, etc.).
- Secure Access: Multi-level user authentication and encrypted alarm logs. These features ensure that every batch is fully traceable, simplifying compliance audits and quality assurance reviews.
Chemical & New Energy Industries: Engineered for Resilience and Safety
In the chemical, pigment, and battery material sectors, ribbon blenders must withstand aggressive environments while handling flammable or high-value materials. Our designs are engineered to meet these extreme operational challenges.
1. Advanced Corrosion Resistance & Material Science
To handle acidic, alkaline, or organic solvent-rich environments, we offer specialized metallurgy and lining options. Beyond standard stainless steel, we utilize Hastelloy, Duplex stainless steel, or PTFE linings. For high-wear applications, the agitator can be configured with a removable liner or bolt-on flighting, allowing for cost-effective maintenance and future material upgrades without replacing the entire shaft.
2. Explosion Protection & Atmospheric Control
When processing combustible dusts—such as carbon materials or metallic powders—safety is paramount. Our equipment is fully compliant with ATEX or NEC explosion-proof certifications. To prevent ignition, systems are equipped with:
- Nitrogen Inerting & Purging: Maintaining a stable, oxygen-free environment.
- Online Oxygen Monitoring: Real-time sensors to ensure the atmosphere remains within safe limits.
- Rated Components: Drive motors, instrumentation, and control enclosures are all rated for hazardous locations (HazLoc).
3. Precision Low-Shear Mixing for High-Value Materials
For sensitive products like battery cathode and anode materials, maintaining particle integrity is as important as homogeneity. To prevent particle degradation (attrition), our blenders utilize:
- Variable Frequency Drives (VFD): For precise control over mixing velocity.
- Low-Shear Ribbon Geometries: Specifically designed to move material efficiently without mechanical damage.
- Soft-Start Systems: Minimizing initial torque impact on both the machine and the product.
4. Large-Scale Automation & System Integration
To support the high-throughput demands of the chemical industry, our blenders—with capacities exceeding 10m³—act as critical nodes within fully automated plants. These units are designed for seamless DCS (Distributed Control System) integration, featuring:
- Closed-Loop Control: Real-time monitoring of humidity, temperature, and particle size.
- Smart Buffering: Serving as a precision pre-mixing or buffer unit to ensure downstream continuity.
Need a specialized mixing solution for your industry? From GMP-compliant pharmaceutical designs to heavy-duty chemical mixers, discover our full range of Advanced Powder Mixing Equipment to find the ideal match for your process.
Key Specifications of Quality Ribbon Blending Machines
When selecting a ribbon blender intended for years of reliable service, the core technical nuances are the ultimate deciders of long-term performance, process alignment, and total cost-effectiveness. While many units may appear identical at first glance, the true value lies in the “hidden” engineering—the structural integrity, material selection, and sealing architecture.
These critical design differences directly dictate your cleaning efficiency, the frequency of maintenance intervals, and, most importantly, the batch-to-batch stability of your final product. Investing in these technical details today prevents operational bottlenecks tomorrow.

Structural Integrity and Metallurgy: SS304, SS316L, and High-Performance Alloys
The material selection for the blender’s main body is the most critical factor in determining its corrosion resistance, structural strength, and operational lifespan. Every selection must be rigorously aligned with both the chemical characteristics of the product and relevant industry standards.
1. SS304 Stainless Steel (General-Purpose & Cost-Effective)
SS304 remains the standard, economical choice for dry, non-corrosive, or mildly reactive environments. It is ideal for bulk chemical powders, flour, and plastic granules. Its surface can be mechanically polished to satisfy basic sanitary requirements without the need for high-end chemical resistance.
2. SS316L Stainless Steel (High-End Sanitary & Corrosive Environments)
As the gold standard for pharmaceuticals and premium food processing, SS316L offers superior durability.1 The addition of molybdenum significantly enhances its resistance to pitting and crevice corrosion—particularly when exposed to chlorides, acidic ingredients, or aggressive CIP (Clean-in-Place) oxidizing agents.3 It is the mandatory choice for direct-contact applications involving active pharmaceutical ingredients (APIs), high-sodium foods, or wet granulation processes.
3. Specialized Material Applications
For extreme operational environments involving concentrated acids, strong bases, or ultra-high-purity requirements, we utilize advanced metallurgy such as Duplex stainless steel or Hastelloy. Additionally, for applications where metal ion contamination must be strictly avoided or where unique chemical resistance is needed, PTFE-lined carbon steel provides an ideal solution for even the most challenging materials.
Surface Treatment and Roughness (Ra Value)
The smoothness of the internal contact surfaces is a critical metric for evaluating a blender’s hygienic integrity, ease of cleaning, and resistance to microbial proliferation. These finishes are quantified by the “Roughness Average” (Ra).
1. Standard Industrial Grade (Ra ≤ 0.8um)
Designed for general food and industrial applications with baseline hygiene requirements. This finish is typically achieved through mechanical polishing and is sufficient for conventional dry-cleaning or wash-down protocols.
2. Sanitary Grade (Ra ≤ 0.4um)
Engineered to meet the stringent mandates of 3-A and EHEDG standards. This near-mirror finish significantly minimizes material adhesion and eliminates microscopic “harborage points.” This is the standard configuration for dairy processing, nutraceuticals, and non-sterile pharmaceutical production.
3. Pharmaceutical/High-Purity Grade (Ra ≤ 0.2um + Electropolishing)
Reserved for sterile pharmaceutical environments or high-potency API (Active Pharmaceutical Ingredient) production. Beyond mechanical polishing, Electropolishing (EP) is utilized to further level the surface profile at a microscopic level. This process creates a dense, uniform passivation layer that drastically enhances corrosion resistance and ensures the highest level of reliability for cleaning validation (CIP/SIP).
Shaft Sealing Technology: The Foundation of Leak Prevention and Operational Life
The integrity of the shaft seal is the single most critical factor in achieving leak-free operation, preventing product contamination, and minimizing maintenance overhead. Depending on the process pressure, material properties, and hygiene requirements, there are three primary sealing technologies:
1. Packing Seals (Traditional & Economical)
As a conventional solution, these achieve a seal by compressing braided graphite or PTFE packing material. While they are cost-effective and can accommodate minor shaft runout, they are characterized by “allowable leakage”—meaning they require periodic tightening and maintenance. They are generally unsuitable for sterile environments or the handling of hazardous and toxic materials.
2. Air Purge Seals (Optimized for Powders)
This is the preferred solution for powder blending. A continuous, low-pressure stream of clean air (or inert gas) is introduced into the seal chamber to create a positive pressure barrier. This prevents fine particulates from migrating into the sealing surfaces, drastically reducing abrasive wear and extending the seal’s service life. It is the ideal configuration for ultrafine powders such as carbon black, pigments, or milk powder.
3. Mechanical Seals (High-Performance & Zero-Leakage)
Mechanical seals represent the gold standard for high-integrity processing. They utilize the precision interface between a rotating and a stationary ring, held together by fluid pressure and spring force, to achieve a near-perfect seal.
- Single Mechanical Seals: Best for atmospheric or slight vacuum conditions.
- Double Mechanical Seals: These utilize a barrier fluid and are designed for fully enclosed, pressurized, or high-vacuum processes (such as solvent mixing and sterile production). Often equipped with leakage monitoring systems, they are the preferred choice for high-standard pharmaceutical and chemical applications.
Selecting the Right Size: Volume vs. Weight
In the procurement process, selecting a mixer based solely on its external dimensions or nominal weight is a common “beginner’s mistake.” Ribbon blenders are fundamentally volumetric devices; therefore, selection must be dictated by material volume, bulk density, and flow characteristics.
Incorrect volume matching does more than just reduce mixing efficiency—it can lead to equipment overload, motor burnout, or total process failure. To ensure an accurate selection, the following two core calculation principles must be applied.
40%–70% Working Volume Rule: Optimizing Convective Flow
Effective blending relies on having sufficient “headspace” to allow for the three-dimensional convective circulation of materials. To ensure a successful selection, it is critical to distinguish between the Total Volume and the Working Volume.
- Total Volume: The maximum theoretical geometric capacity of the U-shaped vessel.
- Working Volume: The actual volume of material processed in a single batch, which should ideally remain within 40% to 70% of the total volume.
1. Impact of Fill Rates
- Underfilling (< 30–40%): If the material level is too low, the product fails to make consistent contact with the upper outer ribbon. This disrupts the convective loop, leading to poor homogeneity and potentially causing shaft vibration due to an uneven distribution of mechanical forces.
- Overfilling (> 70–80%): Excess material severely compresses the internal void space required for shearing and convective movement. This not only drastically extends mixing times and energy consumption but also risks motor stall or transmission failure due to excessive torque demands.
2. Recommended Selection Strategy
Before determining the total volume of the equipment, you should first calculate the volume (not weight) of your single batch of material. It is recommended to reserve approximately 20% of process flexibility space to accommodate future formula or production adjustments. For example, if you need to mix 2 cubic meters of material per batch, you should choose a mixer model with a total volume of approximately 3.3 – 5 cubic meters.
Bulk Density and Motor Power Calibration: Optimizing Torque and Drive Capacity
Bulk density is the primary variable in calculating the required mixing power (HP/kW), as it dictates the total mass and rotational inertia of the material within the vessel. Precise motor matching is essential: underpowered drives will stall under heavy loads, while an oversized motor results in unnecessary energy consumption and inflated capital costs.
1. Standard Configuration (Low-Density Applications)
Optimized for lightweight materials such as flour, starch, milk powder, plastic granules, and most agricultural powders. This configuration focuses on high-speed convective flow and efficient homogenization, utilizing a drive system balanced for energy efficiency and rapid cycle times.
2. Heavy-Duty / High-Torque Configuration
Engineered specifically for materials with high bulk density—including mineral powders, metallic particulates, salt and sugar crystals, and battery anode/cathode materials. To overcome the significant rotational resistance of these substances, the following reinforcements are integrated:
- Reinforced Shaft and Agitator: Utilizes increased wall thickness for the central shaft and reinforced support struts for the ribbons to withstand extreme torsional stress.
- High-Service-Factor Drive Train: Equipped with high-kilowatt motors and heavy-duty gearboxes to provide the necessary breakaway torque for starting under load.
- Enhanced Ribbon Geometry: May feature dual-layered ribbons or reinforced paddle-ribbon hybrids designed to cut through dense material beds without mechanical deflection.
3. Critical Factors for Power Calculation
To ensure operational reliability, suppliers typically utilize empirical formulas to determine the required power based on your material’s peak bulk density and intended working volume. To prevent under-specification, it is essential to provide accurate and comprehensive data regarding the physical properties of your materials—specifically the maximum density and any potential range of fluctuation.
For applications involving exceptionally high densities or specialized viscosities, we strongly recommend conducting a material mixing trial. This practical testing allows engineers to measure actual torque requirements and power draw, ensuring the drive system is precisely calibrated to your specific production environment.
Discharge Solutions for Ribbon Mixers
The discharge phase is a critical link in the mixing cycle. It determines more than just output efficiency; it directly impacts batch homogeneity, material residue levels, and the seamless transition to downstream processing. Selecting a discharge valve is a strategic decision that must account for material flowability, sealing requirements, sanitary standards, and cycle-time targets.
Slide Gate Valves (Horizontal Gate)
Mechanism: A flat plate is driven horizontally across the valve body—via manual, pneumatic, or electric actuation—to open or close the orifice.
- Best For: Free-flowing, non-viscous, and robust particles such as plastic resins, grains, and standard chemical powders.
- Advantages: This is an economical, low-profile solution with a full-bore opening that offers minimal flow resistance and zero shearing of the material.
- Considerations: Sealing performance is basic. It is generally unsuitable for high-vacuum, moisture-sensitive, or oxygen-sensitive applications. Over time, fine powders may migrate into the slide tracks, leading to wear or minor leakage.
Butterfly Valves
Mechanism: A circular disc (butterfly plate) rotates 90° on a central axis to regulate flow. These are available in specialized sanitary designs with various elastomer options (e.g., FDA-approved Silicone, Viton, or EPDM).
- Best For: Food, pharmaceutical, and general chemical applications. It excels with materials prone to “bridging” or semi-solids with slight viscosity, as well as dry powders requiring dust-tight containment.
- Advantages: Rapid actuation, low operating torque, and easy automation. Sanitary versions are engineered for easy wash-downs and reliable sealing.
- Considerations: Even when fully open, the disc remains in the flow path, which can slightly impede a 100% residue-free discharge.
Ball Valves (Full-Bore or Hemispherical)
Mechanism: A spherical core with a hollow center rotates 90° to allow or block flow. In mixing, full-bore V-port or hemispherical designs are common.
- Best For: High-vacuum operations (solvent recovery), pressurized systems, or high-value products where residue must be virtually eliminated (e.g., active APIs or premium pigments).
- Advantages: Offers superior “zero-leakage” sealing and a “no dead space” design. The full-bore aperture ensures unobstructed flow and excellent CIP/SIP compatibility.
- Considerations: This is a higher-cost investment compared to gate or butterfly valves. Highly viscous materials may require significantly higher torque for actuation.
Hatch-Type / Bomb-Bay Discharge Valves
Mechanism: A large section of the trough bottom acts as a high-speed hatch, typically actuated by hydraulic or pneumatic cylinders.
- Best For: Large-scale production and materials with poor flowability (wet agglomerates, viscous pastes). This design is essential when an instantaneous discharge is required to prevent “secondary segregation”—the separation of particles by size or density that can occur during slow, gradual pouring.
- Advantages: Provides the fastest possible discharge with virtually zero residue. By emptying the vessel instantly, it preserves the homogeneity achieved during the mixing cycle and maximizes throughput.
- Considerations: These units are mechanically complex and require a larger footprint. The durability of the large-scale perimeter seals is critical for long-term reliability.
| Dimensions | Slide Gate Valves | Butterfly Valves | Ball Valves | Hatch-Type Discharge Valves |
| Cost-Effectiveness | High | Medium | Medium-Low | Low |
| Sealing Performance | Low | Medium-High | Very High | High |
| Discharge Speed | Medium | Medium | Medium | Very High |
| Residue Prevention | Medium | Medium | High | Very High |
| Anti-Segregation Effect | Low | Low | Medium | Very High |
| Suitable Material Characteristics | Free-flowing, non-sticky materials | Versatile, semi-solids | High-value, closed-system required | Viscous, large-volume, segregation-prone materials |
When making your selection, be sure to consider your material characteristics, process environment (vacuum/pressure), cleanliness standards, production rate, and downstream equipment interfaces. Clearly communicating the valve material, actuator specifications (pneumatic/electric), control method, and spare parts information for the seals with the equipment supplier is essential for ensuring long-term stable operation.
Long-term Stable Operation & Maintenance Management
To ensure that a ribbon blender operates at peak efficiency throughout its service life—and to maximize your Return on Investment. It is essential to implement systematic operating procedures and proactive maintenance strategies. Adhering to these standards does more than just prevent unexpected downtime; it is the fundamental requirement for ensuring batch-to-batch consistency and long-term mechanical reliability.
The Strategic Value of Variable Frequency Drives
In modern ribbon blender design, the Variable Frequency Drive (VFD) has transitioned from an optional feature to a critical control component. Its value extends far beyond simple velocity adjustment, serving as a pillar for both mechanical longevity and process refinement.
1. Soft Start and Mechanical Protection
VFDs facilitate controlled motor acceleration, or “soft starts,” which completely eliminate the destructive impact torque experienced by the gearbox, mixing shaft, and ribbons during direct-on-line starting. This drastically extends the service life of the entire transmission system—a feature that is indispensable when handling high-density materials that offer high initial resistance.
2. Process Optimization and Production Flexibility
- Precision Speed Control: Operators can fine-tune the agitator’s RPM to match specific material characteristics, such as friability or viscosity. This allows for optimal homogenization while minimizing mechanical heat generation or unwanted particle attrition (breakage).
- Multi-Stage Processing: VFDs enable programmable mixing cycles tailored to the product’s lifecycle. For example, a “low-speed dispersion” phase can be followed by “high-speed homogenization,” concluding with a “low-speed discharge” to prevent segregation. These optimized mixing curves ensure superior batch consistency.
3. Energy Efficiency and Intelligent Integration
VFDs dynamically adjust motor output based on real-time load conditions, preventing energy waste during no-load or low-load intervals. Furthermore, integrated communication interfaces (such as Modbus or Profinet) allow for seamless connectivity with factory DCS (Distributed Control Systems) or MES (Manufacturing Execution Systems), facilitating comprehensive data logging and remote process management.
Cleaning Procedures
In industries where quality and safety are paramount, cleaning is more than a hygiene requirement—it is a critical phase of the production cycle that directly influences equipment utilization and uptime.
1. Manual Deep-Cleaning and Complete Disassembly
This approach is ideal for high-mix, small-batch production lines or facilities handling high-risk allergens prone to cross-contamination.
- The Mechanism: High-end blender models often feature quick-release mixing shafts or hydraulic lifting systems. These allow the entire agitator assembly to be removed from the vessel, facilitating meticulous manual scrubbing and 100% visual inspection of all product contact surfaces.
- The Trade-off: While this method offers the highest level of cleanliness assurance, it is labor-intensive and results in longer periods of equipment downtime.
2. Clean-in-Place (CIP) Systems
CIP technology is the standard for modern, continuous production environments. Through automated sequences, cleaning media (water, caustic, or acid solutions) are delivered via rotating spray balls or strategically placed fixed nozzles.
- The Process: The system provides high-impingement rinsing and disinfection across all internal surfaces.
- Key advantages: Significantly reduced batch turnaround time, lower labor costs and operational risks, a traceable and verifiable cleaning process, and full support for pharmaceutical GMP and food safety compliance requirements.
3. Engineering Considerations for CIP
For a CIP system to be effective, several technical parameters must be harmonized:
- Coverage & Impingement: Spray ball positioning must ensure “total wall wash” with no shadow zones.
- Fluid Dynamics: The flow rate, pressure, and temperature of the cleaning media must be strictly maintained.
- System Integration: The blender must be equipped with specialized sanitary piping, high-efficiency pumps, and automated valves that integrate seamlessly into the plant’s central control system.
Diagnostic Insights and Troubleshooting
Developing a rapid response protocol for mechanical issues is essential for minimizing unscheduled downtime. Below are the most frequent operational challenges and their primary root causes.
1. Inconsistent Mixing (Coefficient of Variation Exceeds Limits)
- Primary Cause: Excessive clearance between the ribbon agitator and the vessel wall. Wear over time increases this gap, weakening the critical shearing and convective forces.
- Correction: Regularly inspect the gap and ensure it remains within the design specification—typically 3–5mm.
- Secondary Causes: Improper fill levels (outside the 40%–70% range), significant fluctuations in raw material density, or an incorrect RPM setting on the VFD.
2. Motor Overheating or Nuisance Tripping (Overload)
- Primary Cause: Operating beyond the rated torque capacity. This is usually caused by overfilling the vessel or attempting to process high-bulk-density materials with a “Standard” power configuration.
- Troubleshooting Steps: 1. Verify that the batch weight aligns with the motor’s rated capacity. 2. Review VFD parameters, specifically acceleration ramp times and current limits. 3. Inspect for mechanical resistance, such as seized bearings or foreign object debris (FOD) jamming the agitator.
3. Abnormal Noise or Vibration
Potential Causes: * Bearing Fatigue: Worn or unlubricated main shaft bearings.
- Misalignment: Poor coupling alignment between the motor/gearbox and the drive shaft.
- Structural Integrity: Loose or fractured ribbon support struts or fasteners.
- Contamination: Metal foreign objects or tramp material trapped within the trough.
4. Discharge Valve Leakage or Actuation Failure
Potential Causes: * Seal Degradation: Perished or abraded elastomer seals (common in butterfly valves).
- Material Accumulation: Product “caking” or build-up within the valve seat, preventing a flush closure.
- Actuator Issues: Failure of pneumatic or electric actuators, or insufficient plant air pressure/voltage supply.
Troubleshooting your current system or exploring other mixing options? Understanding the mechanics behind different technologies can prevent future downtime. Read our detailed Guide to the Different Types of Blenders in Pharma for deeper technical insights.
Conclusion: Turning Equipment into a Strategic Asset
An industrial ribbon blender is far more than a simple stainless steel vessel; it is a precision-engineered core process system. Its performance is the primary determinant of the uniformity, stability, and safety of your final product. By aligning your selection with industry compliance standards, scientifically matching volume to power, and implementing standardized operational protocols, you transform this equipment into a strategic asset that guarantees quality and optimizes operational costs.
Reliability as the Cornerstone of Production
In the food, pharmaceutical, chemical, and new energy sectors, the integrity of the mixing process is the foundation of the entire production chain. Choosing a ribbon blender that excels in sanitary design, process adaptability, and technical support provides your production line with lasting stability and the scalability required for future expansion.
Beyond the Initial Quote: Assessing Total Cost of Ownership
When finalizing a procurement decision, looking beyond the “sticker price” is essential. A professional evaluation must encompass the Total Cost of Ownership (TCO) over the equipment’s entire lifecycle, specifically accounting for:
- Energy Efficiency: Optimized motor and VFD performance.
- Maintenance Overhead: Frequency of interventions and spare parts availability.
- Operational Throughput: Cleaning efficiency and batch cycle times.
- Risk Mitigation: The cost of potential production losses or quality failures due to inconsistent mixing.
Investing in a well-designed, seamlessly integrated system that evolves alongside your business is the most effective way to maximize long-term value.
May this guide serve as a roadmap for making informed, forward-thinking decisions, ensuring you select a “strategic partner” that brings efficiency and reliability to your production process for years to come.
Transform your mixing process into a strategic asset with SED Pharma. Our engineers are ready to help you with volume calculations, material trials, and custom configuration designs. Contact Our Technical Experts Today to start your next project with a partner you can trust.