Introduction: Why Blending is the Backbone of Pharma
Mixing is a cornerstone of pharmaceutical manufacturing because it directly dictates a drug’s Critical Quality Attributes: dose uniformity, therapeutic efficacy, patient safety, and batch-to-batch consistency. It’s not simply a physical operation, but a crucial bridge that transforms formula design into safe and effective products.
Modern formulations often contain multiple functional excipients. Mixing must not only distribute the API evenly but also ensure that all excipients are uniformly interwoven at the microscopic level, guaranteeing that the drug disintegrates, dissolves, and is absorbed in the body according to the predetermined design. Mixing connects upstream processes such as raw material grinding and sieving, and downstream processes such as tablet compression, filling, and coating.
Mixing integrates materials science, fluid mechanics, process engineering, and quality control, and is an indispensable core physical transformation process that converts chemical molecules into safe, effective, and reliable drugs. This article, based on the working principles of mixers in the pharmaceutical industry, informs users about the types of materials that can be processed using mixers and analyzes and discusses issues of concern to manufacturers.
How Does Blending Work?
Simply put, the principle of mixing is to use external forces to achieve a uniform spatial distribution of the components in two or more materials. To achieve this goal, mixers utilize three basic microscopic mixing mechanisms, and almost all mixers operate based on a combination of one or more of these three mechanisms.
Convective Mixing
The equipment uses rotation, stirring paddles, and other movements to cause overall, large-scale relative motion of material clumps within the equipment. This rapidly reduces large-scale non-uniformity and is the primary mechanism in the initial stages of mixing.
Diffusive Mixing
Between particle layers, individual particles migrate from one position to another due to random particle motion, local velocity differences, or gravitational sliding. It is responsible for eliminating small-scale differences, ultimately achieving a high degree of uniformity.
Shear Mixing
A velocity gradient is formed within the material. Similar to a deck of cards being fanned out, relative motion occurs between adjacent particle layers, thereby breaking up agglomerates, soft lumps, and arching.

Top Types of Blenders in Pharma
In pharmaceutical manufacturing, there is no single “universal” mixing device that perfectly suits all applications. Based on the physical properties of the materials, production scale, and the required quality standards of the final formulation, pharmaceutical manufacturers must make an optimal choice from a variety of mechanical designs. These devices, through different combinations of convection, diffusion, and shear mechanisms, ensure that even trace amounts of API achieve extremely high uniformity within complex excipient matrices. The following is an analysis of several core mixing technologies currently most widely used in the pharmaceutical industry and their applicability in practical production.
V-type Mixer
The versatility, mixing efficiency, and proven track record of V blender machines make them the preferred choice for pharmaceutical solid powder mixing. Their classic V-shaped cylinder design, during rotation, causes the materials to undergo periodic separation, mixing, and convection, along with diffusion, quickly achieving homogenization of most free flowing APIs and excipients. This makes them suitable for pre-mixing raw materials for tablets and capsules, as well as for large scale production of nutritional supplements. Their relatively simple structure and smooth, dead-space-free interior greatly simplify cleaning and validation processes. When process requirements are clear and the materials are conventional dry powders, choosing a V-type mixer is almost always the most robust and reliable decision.

Double Cone Mixer
Pharmaceutical double cone mixer significantly preserves the integrity of the materials. Its conical design, rotating around a symmetrical axis, creates an extremely gentle, gravity-driven mixing environment. Particles are homogenized through sliding and diffusion, avoiding violent shearing and collisions. It is suitable for processing fragile materials such as coated particles and crystals. Furthermore, its smooth conical inner cavity allows for easy discharge with minimal residue, which not only reduces the risk of cross-contamination between batches but also greatly reduces cleaning difficulty and validation burden. The double cone pharmaceutical blender offers advantages for processes that require high product purity, extreme cleaning efficiency, and where materials are sensitive to shear forces.

Three-dimensional Motion Mixer
The greatest characteristic of a three dimensional motion mixer is that it subjects the materials to a turbulent state similar to “weightlessness” through complex, multi-directional movement in three-dimensional space, achieving a perfect combination of convection and diffusion. Even low-dose APIs can be uniformly mixed with large quantities of excipients, or materials with significantly different densities and particle sizes can be effectively blended. The three-dimensional motion pattern virtually eliminates gravitational segregation, achieving a degree of mixing uniformity that is difficult for other mixers to match. Although it is expensive and typically has a smaller capacity, the three-dimensional motion mixer is a crucial guarantee for achieving quality objectives and ensuring consistent efficacy when developing high-end formulations such as targeted cancer drugs, inhaled powders, and producing high-value products.

Square Cone Mixer
Square cone mixer combines continuous, integrated, and enclosed production technologies, and also features mobility. After mixing is completed in the hopper on the rotating frame, it can be directly lifted to the next process (such as drying or tableting), achieving integrated “mixing-transfer-storage.” This design minimizes material transfer times, fundamentally reducing the risks of dust exposure, cross-contamination, and human error, and is particularly suitable for the stringent safety requirements of high-potency drug manufacturing. The square cone mixer is ideal for solid dosage form factories seeking high efficiency, large-scale, and fully enclosed production processes, significantly improving overall production efficiency and safety levels.

Ribbon Blender
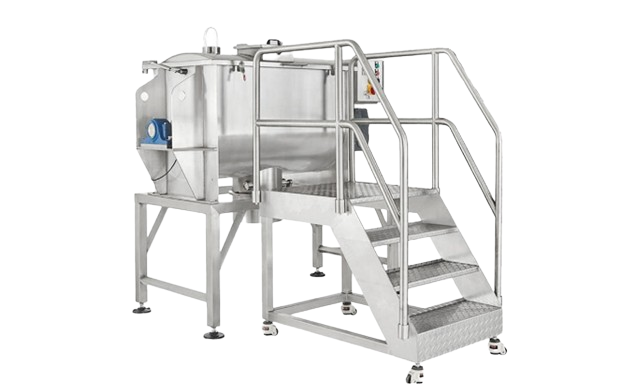
When mixing objects transform from dry powders into semi solid or highly viscous materials such as ointments, creams, and gels, all of the aforementioned gravity-driven mixers are not the optimal choice. The industrial ribbon blender for pharma production utilizes a forced mixing principle; the rotating ribbons or paddles within the horizontal trough generate strong shear forces and axial convection, effectively kneading, cutting, and homogenizing viscous materials. Simultaneously, they are typically equipped with a jacket for precise heating or cooling to meet process temperature control requirements. In the production of topical medications, dermatological preparations, and certain complex ointments, ribbon mixer machines are core equipment for ensuring uniform blending of the base material and API, and for achieving a fine and stable product texture, filling an indispensable gap in the field of pharmaceutical mixing.
| Types | Pros | Cons | Application |
| V Type Blender | 1. Fast mixing speed 2. Simple structure, easy to clean and maintain 3. High industry acceptance and proven technology | 1. Materials with significantly different densities are prone to stratification 2. Viscous and easily caking materials do not yield good results. | 1. Pre-mixing of the API and excipients for tablets/capsules 2. Final blending of the free-flowing granules |
| Double Cone Blender | 1. Gentle mixing process preserving the integrity of the particles 2. Thorough discharge, with minimal residue 3. No dead corners, simple cleaning and validation | 1. Slow mixing speed 2. Not suitable for viscous materials | 1. Mixing of granules before coating 2. Gentle mixing of low-melting point or crystalline raw materials |
| Three-dimensional Motion Mixer | 1. High mixing uniformity without stratification 2. Different density and particle size acceptable 3. Ideal for low additive concentrations | 1. High price 2. Complex structure 3. Small loading capacity | 1. Micro-mixing of highly active drugs 2. R&D or production of drugs in small clinical batches |
| Square Cone Mixer | 1. Integrated mixing, transfer, and storage 2. Low pollution and dust risk | 1. High initial investment 2. Lower uniformity than that of V-type or double cone mixers | 1. Large scale batch production in solid dosage form 2. Mixing needed in closed production processes |
| Ribbon Blender | 1. High viscosity, semi solid, and paste capable 2. High mixing intensity | 1. Complex structure with hard-to-clean areas 2. Excessive shearing may occur | 1. Ointments, creams, and gels 2. Wet granules |
SED Pharma works as a professional mixing machine manufacturer for pharmaceutical industry. We not only manufacture equipment, but also provide mixing solutions that meet the stringent requirements of cGMP validation – from classic V-type mixers to enclosed systems designed specifically for highly active pharmaceutical ingredients. Each piece of equipment embodies our deep understanding of pharmaceutical processes. Explore the SED Pharma mixing equipment series today.
What Users Are Asking about Blenders?
Q1: What Are the Key Process Parameters that Affect the Mixing Effect?
A1: Mixing effectiveness is not solely determined by the equipment; process parameter settings are equally important. Key parameters include:
- Loading Quantity (Loading Factor): This is one of the most important parameters. Too high or too low a loading quantity will severely affect mixing dynamics. The optimal range is typically 30% to 70% of the total equipment volume, which needs to be determined through validation.
- Rotation Speed: This determines the energy of material movement. Too low a speed results in insufficient mixing; too high a speed may lead to centrifugal effects, particle breakage, or excessive frictional heating. A balance between efficiency and material integrity needs to be found.
- Mixing Time: Longer is not always better. After reaching optimal homogeneity, continued mixing may lead to “reverse mixing” (segregation). The shortest effective mixing time needs to be determined through process validation (e.g., sampling and analysis at different time points).
- Material Characteristics: These include particle size distribution, particle shape, density, flowability, electrostatic properties, and viscosity. This is the fundamental basis for selecting equipment and setting parameters. For example, materials with large density differences require longer diffusion mixing times.
- Mixing Order (Addition Order): For multi-component mixing, especially when there are trace amounts of active ingredients, the geometric dilution method is recommended: pre-mix the trace component with an equal amount of excipient, and then gradually mix this mixture with the remaining excipients to ensure uniform distribution.
- Equipment Internal Structure: This includes the presence of baffles, choppers, or liquid spraying devices. These can break up agglomerates, enhance shear, or facilitate solid-liquid mixing.
Q2: How to Determine the Optimal Loading Capacity for A Mixer?
A2: The optimal loading volume needs to be determined through systematic process validation, which is a scientific process, not an estimation. The recommended steps are as follows:
- Design a mixing uniformity test: Conduct tests at a fixed rotation speed and mixing time, using three loading levels (e.g., 30%, 50%, 70%).
- Select a tracer and analytical method: Use a “placebo” material similar in properties to the actual material, adding a small amount of tracer (such as a dye or API analog). Perform multi-point sampling and analysis using a content uniformity method (HPLC) or a physical method (near-infrared spectroscopy NIR).
- Evaluate the results: Calculate the mixing uniformity for each loading volume (evaluated by relative standard deviation RSD or mixing index M). The loading volume with the smallest RSD value and the mixing index closest to 1 is the theoretically optimal value.
- Consider actual production: The final determined loading volume should also consider production batch requirements, ease of cleaning, and the robustness of the mixing effect at different loading volumes.
Q3: What Are the Cleaning Requirements for Pharmaceutical Mixing Equipment?
A3: The core of cleaning requirements is preventing cross-contamination and ensuring product safety, and must be based on risk assessment and validation.
Regulatory Basis: Must comply with cGMP requirements, particularly guidelines for cleaning validation.
Cleaning Limit Standards:
- Visual Cleanliness: No visible residue on all contact surfaces.
- Chemical Limits: The maximum allowable residue of the previous product’s active ingredient on the equipment surface is calculated based on a standard of 1/1000 of the daily therapeutic dose or 10 ppm. The stricter standard of the two is used.
- Biological Limits: If necessary, microbial and bacterial endotoxin testing should be performed after cleaning.
Cleaning Methods:
- Cleaning Out of Place (COP): Removable parts (such as hoppers, paddles) are moved to a cleaning station for cleaning. Suitable for small or structurally complex equipment.
- Cleaning In Place (CIP): The inside of the equipment is automatically cleaned using detergents and purified water/water for injection through a pre-set program and spray balls. This is the preferred method due to its standardization, recordability, and reduced personnel exposure.
- Cleaning Validation: The effectiveness and reproducibility of the cleaning procedure must be demonstrated through three consecutive successful cleaning validations. The validation protocol must clearly define the worst-case conditions (most difficult product to clean, longest retention time, etc.).
Q4: How Are CIP and SIP Systems Implemented on Mixing Equipment?
A4: The two cleaning methods key design feature of modern pharmaceutical mixing machines.
CIP Implementation Methods:
- Spraying System: Fixed or rotating spray balls are installed at the top of the mixer or at critical locations to ensure that the cleaning solution covers all contact surfaces.
- Piping and Interfaces: The equipment is equipped with standardized quick-connect interfaces for connection to the CIP station, used for conveying cleaning agents, water, and compressed air.
- Automated Program: Controlled by a PLC, it automatically executes steps such as pre-rinsing -> alkaline washing -> intermediate rinsing -> acid washing (optional) -> final rinsing -> drying, and records key parameters (time, temperature, conductivity, flow rate).
SIP Implementation Methods:
- Design Premise: The equipment must be a closed, pressure-resistant system, and all seals must withstand high temperature and pressure.
- Sterilization Medium: Typically uses pure saturated steam. Superheated water or hydrogen peroxide vapor can also be used.
- Key Points: The system needs steam traps to drain condensate, and temperature sensors are installed at the coldest points that are most difficult to heat, ensuring that these points reach and maintain the sterilization temperature and time. All piping designs must avoid condensate accumulation.
Q5: How to Monitor the Mixing Homogeneity during the Mixing Process?
A5: The goal of online sampling is to obtain representative samples without disrupting the mixing process, introducing contamination, or creating safety risks.
Safety and Compliance First:
For highly active pharmaceutical ingredients: A completely closed sampling system must be used, operating under negative pressure or within an isolator to prevent dust exposure.
Follow SOPs: Any sampling operation must have an approved Standard Operating Procedure.
Sampling Equipment and Methods:
- Dedicated Sampling Valve/Port: The equipment should be designed with a validated sampling valve. The valve opening should be smooth, free of dead spaces, and easy to clean.
- “Sampling Gun” Method: During a pause in mixing, a dedicated sampling probe with multiple compartments or a specific geometric structure is inserted from predefined locations in the mixing vessel to collect samples from multiple points. This is the most scientific method.
- Sampling Timing and Quantity: Samples should be taken at the beginning, middle, and end of the mixing process. The number of sampling points should be statistically significant, usually no fewer than 10.
Core Principle: The sampling operation itself should not interfere with the randomness of the mixing process. Samples should not be taken only from easily accessible locations; otherwise, the results will not be representative.
Conclusion & Future Outlook
Choosing the right blender is more than a procurement decision; it’s a strategic investment in product quality, process efficiency, and regulatory compliance. From the versatile V-type blender to the precision-engineered three-dimensional motion mixer, each type serves a distinct and critical role in the modern pharmaceutical manufacturing landscape. The decision hinges on a deep understanding of your specific material properties, production scale, and quality targets.
As the pharmaceutical industry evolves, so do the technologies underpinning critical processes like mixing. The future points toward greater intelligence, integration, and control:
Continuous & Integrated Processing: The shift from traditional batch mixing toward continuous manufacturing is accelerating. This demands equipment that can integrate seamlessly into a continuous line, offering real-time monitoring and control. Square cone (IBC) systems are leading this charge by acting as mobile process vessels.
Smart Manufacturing & Digitalization: The era of Industry 4.0 is transforming mixing from a black-box operation into a data-rich, transparent process. Future mixers will be equipped with advanced Process Analytical Technology, such as in-line NIR probes, providing real-time feedback on blend uniformity and enabling automated, closed-loop control.
Enhanced Containment & Safety: With the growth of highly potent active pharmaceutical ingredients, the demand for inherently safe design will intensify. Expect to see wider adoption of fully contained systems with integrated CIP/SIP, advanced isolation technologies, and designs that minimize operator exposure and environmental release.
Sustainability & Efficiency: Energy-efficient designs, reduced waste through optimal discharge, and the use of advanced, cleanable materials will become standard expectations, driven by both economic and environmental goals.
At SED Pharma, we are not just observers of these trends; we are active participants in shaping this future. We combine decades of engineering expertise in pharmaceutical-grade mixing with a forward-looking approach to technology. Whether you are scaling up a novel therapy or optimizing a high-volume production line, our team is ready to partner with you to select, validate, and implement the mixing solution that meets today’s demands and is ready for tomorrow’s challenges.
Ready to specify the ideal mixer for your next project or to modernize your existing process?