Introduction
Within pharmaceutical manufacturing, the packaging of capsules and tablets is a critical link in ensuring long-term stability and medication safety. Faced with APIs that are increasingly sensitive to external elements, pharmaceutical companies must navigate the practical challenge of selecting the right protective environment for their products.
Traditional blister packaging is economical and meets the conventional needs of most solid doses. In contrast, Alu Alu packaging provides a superior shield for drugs highly susceptible to degradation from oxygen, light, and humidity. We will systematically compare these two formats across technical structures, barrier performance, and overall ROI to provide an objective reference for your product development and packaging decisions.
What is Alu Alu and Standard Blister Packaging?
To understand the comparison, we must first look at the “anatomy” of these two packaging giants.
Alu Alu (Cold Form Foil)
Alu Alu (Cold Form Foil) is the industry’s go-to solution for high-barrier protection. Designed for medications that can’t afford a single “bad day” of exposure, its opaque, plastic-free appearance offers near-absolute isolation from the outside world.
What makes Alu Alu Foil so effective? It’s all in the layers:
- OPA (Outer Layer): Think of this as the “armor” that prevents punctures and tears.
- Aluminum (The Core): This is the ultimate barrier. It stops moisture, light, and oxygen dead in their tracks.
- PVC (Inner Layer): This ensures your blister pack stays tightly sealed until the moment the patient opens it.
Unlike standard blisters that use heat, Cold Forming uses mechanical pressure at room temperature. This is a game-changer for sensitive drugs, as it eliminates the risk of heat damage during the packaging phase. It’s no surprise that this is the primary choice for biologics and highly active compounds.

Standard Blister (Thermoforming)
Standard Blister Packaging is the “industry workhorse” for tablets and capsules. Valued for its versatility and cost-effectiveness, this format pairs a transparent plastic base with a secure aluminum foil seal, providing a clear view of the medication while maintaining its integrity.
The foundation of this package is the thermoforming process. By heating the plastic film (most commonly PVC) to its softening point, manufacturers can mold individual cavities that perfectly cradle each dose. For products that require more than just basic protection, high-barrier options like PVC/PVDC or Aclar-laminated films are used to shield against environmental humidity.
This flexibility makes thermoformed blisters the go-to choice for the majority of OTC and generic medications. By adjusting the coating—such as adding a PVDC layer—companies can achieve the perfect balance between cost-efficiency and the specialized barrier properties required to keep their medications safe throughout their shelf life.
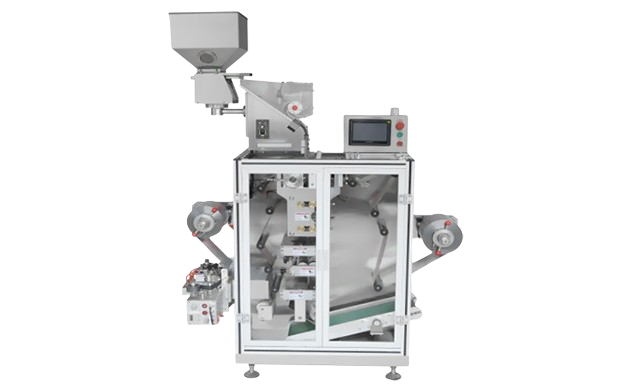
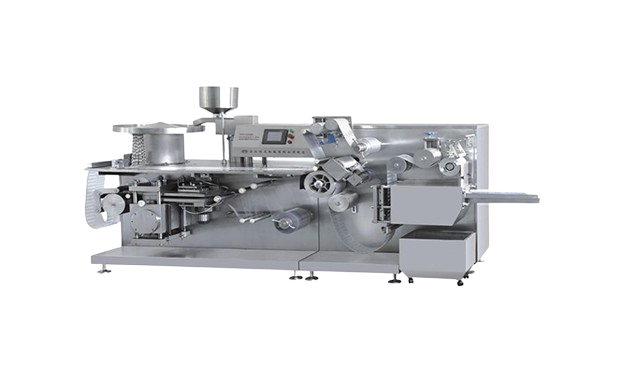
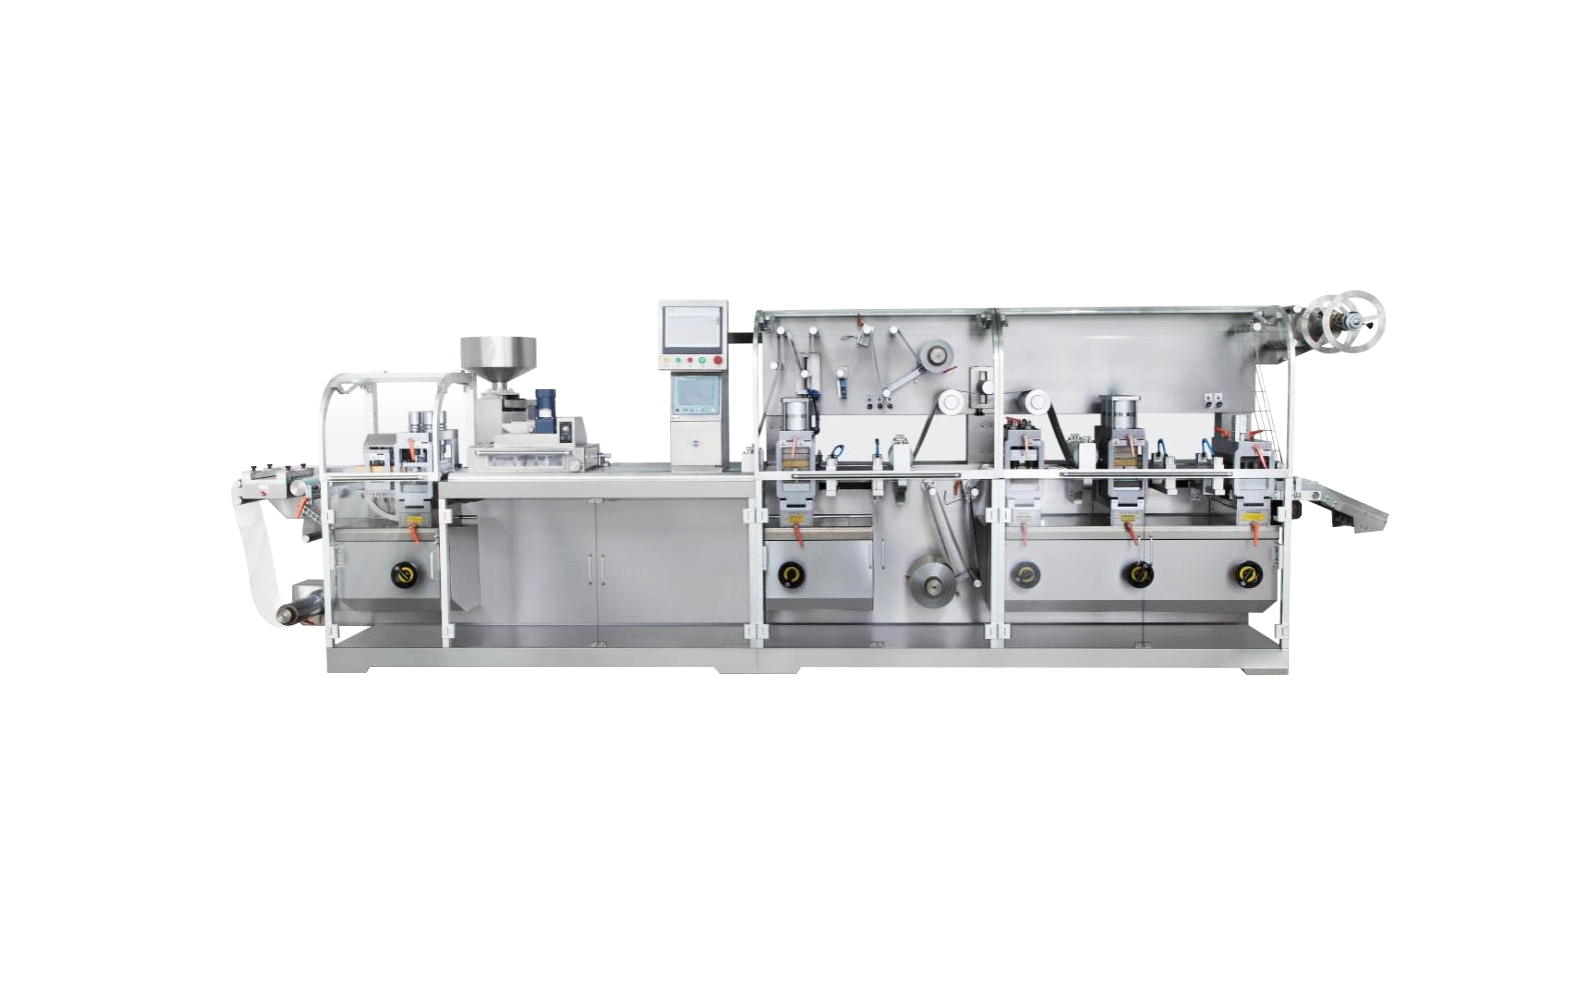
By heating the plastic film to its softening point, manufacturers can mold individual cavities that perfectly cradle each dose. This thermoforming process is enabled by precision blister packaging machines, which ensure consistent cavity formation, reliable sealing, and high-speed output for both standard and high-barrier film types.

Total Barrier vs. Clear Cavity
When evaluating product integrity, the choice of packaging is fundamentally dictated by the chemical stability and degradation profile of the drug.
Maximum Barrier Protection for Sensitive Formulations
For hygroscopic or photosensitive Active Pharmaceutical Ingredients (APIs), Alu-Alu (Cold Form Foil) is the gold standard due to its near-absolute barrier properties.
The Zero-Ingress Standard: Its all-aluminum architecture—utilizing both an aluminum substrate and lidding foil—achieves a near-zero Moisture Vapor Transmission Rate (MVTR) and Oxygen Transmission Rate (OTR). This creates a hermetically sealed, stable microenvironment for volatile molecules.
Total Opacity: Alu-Alu provides a 100% light shield, effectively neutralizing the risk of photo-degradation in light-sensitive compounds.
Transparency and Patient Compliance
The primary advantage of Standard Blister Packaging (Thermoformed) lies in its visual clarity.
Visual Dose Verification: Transparency allows patients to verify at a glance whether they have taken their dose. This visual cue is a critical factor in patient compliance, particularly for the elderly or those managing complex multi-drug regimens.
Consumer Trust and Brand Recognition: For Over-the-Counter (OTC) products, the ability to see the tablet’s shape, color, and branding builds immediate consumer confidence and aids in rapid product identification on the shelf.
Strategic Recommendations
For High-Potency and Labile Drugs: If your formulation includes biologics, easily hydrolyzed compounds, or photodegradable APIs, Alu-Alu packaging is a strategic necessity to ensure safety and efficacy throughout the product’s shelf-life.
For Stable Generics and OTCs: If the drug is chemically stable and has lower barrier requirements, Standard Blister Packaging is the ideal choice. It offers a perfect balance of cost-efficiency, patient convenience, and market appeal.
Manufacturing & Operational Efficiency
Evaluating packaging costs requires a holistic perspective that extends beyond raw material prices to include production throughput, equipment uptime, and long-term mechanical performance.
Production Throughput and Tooling
Thermoforming (standard blister packaging) generally holds a significant speed advantage. As a mature technology, high-speed blister packaging machines are capable of producing thousands of units per hour. It achieves high output through advanced blister packaging machines designed for rapid heating, precise molding, and consistent sealing—key for cost-sensitive high-volume production.
In contrast, cold forming Alu Alu equipment typically operates at a more measured pace. Because the aluminum foil must withstand extreme mechanical stress during the stamping process, higher precision and a stabilized forming rhythm are required to prevent micro-cracking. This necessity for structural integrity results in a comparatively longer production cycle.
Layout Efficiency and Packaging Size
The inherent characteristics of the base materials directly impact layout density and total packaging volume.
- Plastic Polymers: Due to their excellent fluidity and flexibility during thermoforming, plastics allow for steep-walled cavities and tight nesting arrangements, maximizing space utilization on the forming web.
- Aluminum Foil: Cold stamping requires a specific radius of curvature to prevent material failure during stretching. This physical constraint makes it challenging to achieve a compact layout.
When packaging the same number of tablets, this disparity leads to:
Increased Dimensions: Alu-Alu blister cards are typically 30%–50% larger than their plastic counterparts.
Downstream Cost Impacts: Larger cards necessitate larger secondary packaging (cartons), which compounds costs across warehousing, logistics, and transportation.
The performance of your blister packaging line—whether for high-speed thermoforming or precision cold-forming—relies on equipment that balances speed, accuracy, and cost.
At SED Pharma, we design packaging machines that deliver both efficiency and control, supporting everything from standard PVC blisters to high-barrier Alu Alu applications. Our solutions help optimize output, minimize waste, and scale with your needs.
The Bottom Line
Selecting the optimal packaging process requires a multidimensional evaluation. To achieve the perfect balance between cost-control and product requirements, manufacturers must weigh production speed and layout efficiency against the downstream logistics of the final product.
ROI in Pharmaceutical Packaging
When evaluating pharmaceutical packaging, the primary question is whether the premium price of Alu-Alu packaging justifies the investment. To answer this, we must look beyond initial procurement costs and analyze the Return on Investment (ROI) across three critical dimensions.

The Cost Reality: Material and Footprint
It is undeniable that Alu-Alu carries a higher price tag. The raw material—multi-layer composite coldform foil—is significantly more expensive than standard PVC or PVDC films. Furthermore, due to the mechanical requirements of the cold-forming process, the blister layout is typically less compact. With a surface area per unit dose averaging 30%–50% larger than standard blisters, the direct material cost per dose can be 2 to 3 times higher.
Key Return: Maximizing Product Shelf Life
The primary “interest” on this investment is enhanced stability. In high-temperature and high-humidity regions (specifically ICH Climate Zones III and IV, such as Southeast Asia and Latin America), conventional blister packaging often limits drug shelf life to roughly 12 months.
In contrast, Alu-Alu provides a near-zero permeability barrier against moisture, oxygen, and light. This superior protection can extend shelf life to 36 months or more, providing a massive competitive advantage and greater flexibility in global distribution.
Hidden ROI: Resilience and Risk Mitigation
Beyond shelf life, Alu-Alu offers “hidden” financial benefits by reducing Supply Chain Risk:
- Reduced Spoilage: Longer shelf life drastically minimizes losses from expired or degraded inventory.
- Environmental Buffering: It acts as a safeguard against environmental fluctuations during transit and storage in unpredictable climates.
- Stock-out Prevention: By stabilizing the supply chain, it reduces the risk of market shortages.
Additionally, the reliability of your blister packaging line itself is a critical factor in mitigating operational risk. Modern, well-calibrated blister packaging machines minimize downtime, reduce material waste due to sealing errors or cavity defects, and ensure consistent output quality—directly supporting the long-term ROI of both standard and high-barrier packaging formats.
Table 1: Differences of Alu Alu and Blister Packaging
| Feature | Alu Alu (Cold Form Foil) | Standard Blister (PVC/PVDC) |
| Material Structure | OPA / Aluminum / PVC | PVC or PVC/PVDC / Aclar |
| Barrier Property | Excellent (Water, Oxygen, Light) | Good to Moderate |
| Visibility | Opaque (Cannot see product) | Transparent / Translucent |
| Cost | Higher (Material & Production) | Lower (Cost-effective) |
| Production Speed | Slower (Mechanical Stamping) | Faster (Thermoforming) |
| Best For | Moisture/Light sensitive drugs | Stable drugs, OTC products |
Technical Specifications & Model Selection for Blister Packaging Lines
When scaling from laboratory trials to commercial production, the choice of blister packaging machinery directly impacts throughput, material compatibility, and overall equipment effectiveness (OEE).
For Alu-PVC thermoforming applications, the SED-P-A series offers production capacities ranging from 1,800 to 3,000 plates per hour. It features a maximum forming area of 390×150 mm² and a forming depth up to 50 mm, accommodating various tablet and capsule sizes.
For high-speed Alu-PVC operations, the SED-260P-A model achieves punch frequencies of 20–50 cuts per minute (Alu-Plastic) with a maximum forming size of 250×110×15 mm.
In contrast, Alu-Alu cold-forming typically operates at 15–25 cuts per minute due to the mechanical stamping process requirements. SED Pharma’s blister packaging machines feature ±0.1 mm mold tolerance and ±1°C temperature control precision, ensuring consistent cavity formation and seal integrity across both packaging formats.
The quick-change mold system enables rapid format switching between Alu-PVC and Alu-Alu materials within the same production line, reducing changeover downtime.
For quality assurance, SED offers integrated vision inspection systems (SED-PZSJ-B series) capable of double-sided defect detection at speeds up to 800 plates per minute, automatically rejecting non-conforming packs before they reach secondary packaging.To discuss your specific output requirements or request a customized layout design, contact our engineering team for a free quote.
Conclusion
Choosing between Aluminum-Aluminum (Alu-Alu) and standard blister packaging is essentially a strategic exercise in balancing product integrity, cost-efficiency, and environmental stewardship. A systematic evaluation should be guided by the following key pillars:
Precision Engineering Based on Stability Profiles
The first step is a data-driven determination of the product’s specific barrier requirements derived from stability testing. It is crucial to identify whether the API (Active Pharmaceutical Ingredient) necessitates an “absolute barrier” to maintain its shelf life, or if high-barrier coatings and composite films are sufficient. Striking this balance avoids the dual pitfalls of “over-packaging” (which inflates costs) and “under-protection” (which compromises safety).
Strategic Adaptability for Target Markets
Geography dictates packaging strategy. For products destined for ICH Climate Zones III and IV (e.g., Southeast Asia, South America), the superior moisture and oxygen barrier of Alu-Alu can be the deciding factor in whether a drug remains viable throughout its lifecycle. Conversely, for markets with temperate climates and highly regulated, climate-controlled distribution chains, standard blister packaging often provides an optimal and sufficient solution.
Life-Cycle Costs and Sustainability
Moving beyond initial procurement, a true Total Cost of Ownership (TCO) analysis must account for the financial gains of extended shelf life, reduced product wastage, and the potential for improved patient compliance through better therapeutic outcomes.
Furthermore, today’s packaging decisions must integrate Environmental, Social, and Governance (ESG) goals. This includes evaluating the investment required for material recyclability and ensuring full compliance with increasingly stringent global environmental regulations. In the modern pharmaceutical landscape, packaging selection has evolved from a purely technical task into a strategic and socially responsible mandate.
Final summary in pharmaceutical packaging, there is no universal “best”—only the “most suitable.” We recommend that organizations implement a systematic evaluation framework that integrates drug characteristics, market environmental data, cost structures, and sustainability milestones. By doing so, companies can achieve a “win-win” synergy: maximizing economic returns and corporate social responsibility while ensuring the uncompromising safety and efficacy of the medication.
FAQ: Blister Packaging Line Selection & Integration
Q1: What is the typical lead time for a custom blister packaging line from SED Pharma?
Standard SED-P series blister packaging machines have a lead time of 30–45 days. Customized configurations (e.g., specialized feeders, integrated vision inspection, or secondary packaging integration) may extend this to 60–90 days. Our team provides a detailed project timeline upon specification confirmation.
Q2: Can the same blister packaging machine handle both Alu-Alu and Alu-PVC materials?
Yes. SED Pharma’s blister packaging machines are designed with interchangeable forming stations—thermoforming for Alu-PVC and cold-forming tooling for Alu-Alu. The SED-GP series high-speed rotary blister machine supports both material types with quick mold changeover, typically under 30 minutes. However, production speeds differ: Alu-PVC runs at 20–50 cuts/min, while Alu-Alu operates at 15–25 cuts/min due to the mechanical stamping process.
Q3: What are the utility requirements (power, air, water) for a typical blister packaging line?
For a standard SED-260P-A model (Alu-PVC/Alu-Alu): power supply is 380V 50Hz at 8kW, compressed air requirement is ≥0.25 m³/min at 0.6–0.8 MPa, and cooling water consumption is 60–100 L/hr. Larger models like SED-350P-A require 9.5kW power and ≥0.6 m³/min air compression. Our engineering team provides a detailed utilities checklist during the pre-installation phase.