Pharmaceutical manufacturers hit this question early in every drug development project: capsule or tablet? It sounds simple. It isn’t. The answer ripples through bioavailability, patient compliance, production line setup, and per-unit cost. Both are solid oral dosage forms and together make up about 80% of all prescription and OTC medications. But the engineering, chemistry, and economics behind each path are different enough that picking the wrong one can mean expensive reformulation work and equipment retrofitting later.
Capsules and tablets do the same job, but they differ in shell composition, manufacturing process, absorption speed, taste-masking capability, and total production cost. Capsules dissolve faster, are easier to swallow, and work well for small-batch manufacturing with a capsule filler machine. Tablets are more stable, pack higher dose precision, cost less per unit at scale, and handle modified-release profiles better through advanced coating. There is no universal winner. It depends on your API, your patients, your volume, and your budget.
Below is how capsules and tablets stack up across the dimensions that matter most.
Manufacturing Process: How Capsules and Tablets Are Made

Capsule manufacturing fills pre-formed shells with powder, pellets, or liquid. Tablet production compresses granulated powder under high pressure with a tablet press, then optionally coats the result.
Capsule Production Workflow
Capsule manufacturing runs manual, semi-automatic, or fully automatic. It starts with empty capsule shells made from gelatin or hydroxypropyl methylcellulose (HPMC). These come in two interlocking halves: body and cap.
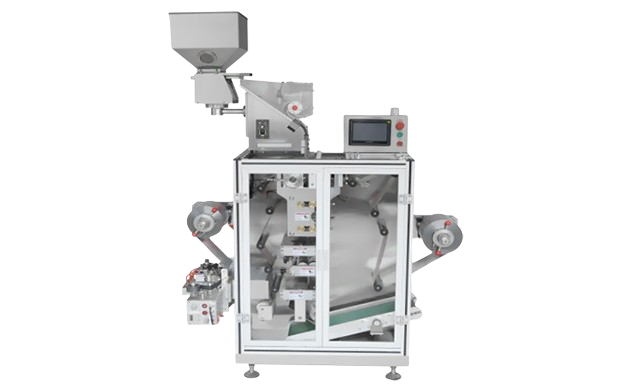
A capsule filler machine separates the halves, doses the fill into each body, then rejoins and locks them. Semi-automatic machines do 300 to 3,000 capsules per hour. Fully automatic units push past 100,000. Fill material can be powder, granules, pellets, tablets, or liquid.
After filling, capsules go through a polisher to knock off surface dust and loose powder. Gelatin capsules especially need this, since residual powder causes sticking during packaging. Polishing uses a rotating brush or vacuum drum—and the trick is cleaning the capsule without cracking the shell.
Vision inspection systems then check each capsule for dents, splits, incomplete closure, size variation, and color problems. A good modern machine can inspect tens of thousands per hour and kick out rejects with compressed air.
Tablet Production Workflow
Tablet manufacturing has more steps but hits much higher speeds at scale. Three stages: granulation, compression, coating.
Granulation turns API and excipient powders into free-flowing granules that compress evenly. Wet granulation uses a liquid binder followed by drying. Dry granulation slugs the powder under pressure and mills it into granules. The choice comes down to how much moisture and heat the API can handle.
Compression feeds granules into a die cavity and squeezes them between two punches. Small tablets need a few kilonewtons. Large industrial tablets can take over 100 kN. Rotary presses dominate here, with turrets carrying 16 to 67 stations and putting out 50,000 to more than 500,000 tablets per hour. Single-punch eccentric presses handle R&D and tiny batches.
After compression, many tablets get coated. Film coating adds a thin polymer layer that masks bitterness, blocks moisture, or controls when the drug releases. Enteric coating keeps the tablet intact through the stomach. Sustained-release coatings meter the API over hours.
QC checks the cap for weight variation, thickness, hardness, friability, disintegration time, and visual defects such as chips, cracks, and foreign particles. Automated visual inspection machines grab multiple images per tablet at speed and use machine vision to flag anything off.

Key Equipment Comparison
| Process Step | Capsule Equipment | Tablet Equipment |
|---|
| Shell / granule preparation | External shell supplier | Granulator (wet or dry) |
| Core forming | Capsule filler machine | Tablet press (rotary or single-punch) |
| Surface finishing | Capsule polisher | Tablet coating machine (film, enteric, sugar) |
| Quality inspection | Capsule inspection (visual) | Tablet inspection (visual + hardness + friability) |
| Typical max throughput | 100,000-200,000 capsules/hour | 300,000-500,000+ tablets/hour |
Bioavailability and Absorption: Which Delivers Faster?
Capsules dissolve faster than uncoated tablets and much faster than film-coated or enteric-coated ones. The gelatin or HPMC shell ruptures within minutes of hitting gastric fluid.
Gelatin capsules start softening 2-4 minutes after entering the stomach and break open shortly after that. Fill material dumps directly into the gastric environment. This is why analgesics, anti-migraine drugs, and anything where speed counts often go the capsule route.
Tablets have more work to do. They have to disintegrate from a compressed solid into granules, then into fine particles, before the API dissolves. Uncoated immediate-release tablets take 15-30 minutes under USP conditions. Film coating adds time. Enteric-coated tablets wait until they hit the small intestine, which can take 1-3 hours.
Liquid-filled capsules are an interesting case. The shell dissolves and the API is already in solution or suspension, so bioavailability approaches what you’d get from an oral solution.
But the capsule advantage isn’t absolute. A formulator with the right disintegrants and compression settings can make immediate-release tablets that match capsule dissolution speeds. And orally disintegrating tablets dissolve on the tongue in seconds, no water needed. Capsules can’t match that.
Taste Masking and Patient Acceptability
Capsules mask taste naturally because the shell completely encloses the API. Tablets need a coating layer for the same effect, which adds a step and cost.
Bad taste is one of the top three reasons patients stop taking their medication. Pediatric and geriatric patients are the hardest hit. Capsules solve this with structure alone: the shell is a physical barrier between the API and the tongue. As long as the patient doesn’t break or chew it, the taste stays locked inside.
Uncoated tablets dump API and excipients right onto the tongue. A lot of APIs are bitter, and even excipients like magnesium stearate leave a lousy mouthfeel. Coating fixes this with a thin polymer film that adds only 2-4% to tablet weight. Sugar coating adds 10-50% and is falling out of favor, but it still shows up in some chewable and pediatric products.
Swallowing matters too. Capsules in sizes 0 through 3 have a smooth, tapered shape that slides down the esophagus easily. Tablets can be made with beveled edges, but angular edges and larger diameters still trip some people up. Patients with dysphagia can sometimes open capsules or crush tablets, but you have to check the release profile first—crushing a modified-release form can cause dose dumping.
Stability and Shelf Life
Tablets are more chemically and physically stable than capsules. The compressed matrix protects the API from moisture and oxygen better than a thin gelatin shell.
ICH guidelines require proof that a drug product holds its identity, strength, quality, and purity across its labeled shelf life. Tablets win on stability, and the margin isn’t small.
Moisture is the biggest problem for gelatin capsules. Gelatin holds 13-16% water and trades moisture with the environment constantly. Drop the humidity, and capsules go brittle and crack. Push it above 60% RH, and they soak up water, soften, and can cross-link. Cross-linking slows dissolution and cuts bioavailability. HPMC capsules handle moisture better but still fall short of compressed tablets.
Film-coated tablets shrug off a wider band of temperature and humidity. The compaction step creates a dense, low-porosity matrix, and a tablet coating adds a moisture barrier on top. Tablets often ship in standard blister packs or bottles with no desiccant. Capsules usually need desiccant and heavier packaging, which drives up cost.
Oxidation hits both forms but in different ways. Oxygen seeps through capsule shells over time, HPMC worse than gelatin. In tablets, tight compression limits internal oxygen exposure, and the film coating can include oxygen-barrier polymers for sensitive APIs. Light sensitivity also favors tablets. Translucent gelatin capsules offer almost no UV protection. Tablets can be formulated with titanium dioxide and iron oxides and coated opaque to protect light-sensitive APIs across the full product lifecycle.
Production Economics: Cost per Unit at Scale

Tablets become cheaper than capsules once you cross roughly 5-10 million units per year. Higher throughput, cheaper raw materials, and simpler packaging drive the difference.
Raw material costs make the case quickly. Gelatin capsule shells run $3-15 per thousand. HPMC runs $5-20. Tablet excipients—fillers, binders, disintegrants, and lubricants—cost $0.50-3.00 per thousand. At 100 million units a year, shell costs alone top $1 million, while the equivalent tablet excipients come in under $100,000.
Equipment throughput pushes the same direction. A single rotary tablet press, sitting in about 4 square meters, cranks out 400,000-500,000 tablets per hour. The best automatic capsule fillers hit 150,000-200,000 per hour and need more complex mechanics for shell handling, separation, filling, and rejoining. Add auxiliary gear like a capsule polisher and dust extraction, and the line footprint and capital cost keep climbing.
Packaging also favors tablets. Capsules are more fragile. They need gentler handling during counting and blister packing and run slower because they are lighter and pick up static. Blister cavities for capsules have to be deeper, burning through more forming material.
| Annual Volume | Capsule Cost per 1,000 | Tablet Cost per 1,000 | Savings with Tablets |
|---|
| 500,000 | $28-42 | $32-48 | Tablets are more expensive |
| 5,000,000 | $22-35 | $18-28 | 18-20% savings |
| 50,000,000 | $15-25 | $8-14 | 40-44% savings |
| 500,000,000 | $10-18 | $4-8 | 55-60% savings |
These numbers include materials, labor, depreciation, utilities, and QC testing. The exact crossover depends on formulation complexity and local labor rates, but it lands between 5 and 10 million units for most products.
Modified-Release Capabilities
Tablets cover more modified-release ground than capsules. Matrix systems, osmotic pumps, multi-layer compression, and functional coating are all tablet territory. Capsules mostly work through pellets.
Modified-release delivery stretches patent life, cuts dosing frequency, and opens up new therapeutic windows. Tablets lead here because the manufacturing toolkit is just bigger.
Matrix tablets embed the API in a polymer matrix that erodes or swells over 8-24 hours. HPMC hydrophilic matrices form a gel layer on contact with water that controls diffusion. Wax-based hydrophobic matrices release through erosion. Both approaches run on standard presses with no extra equipment.
Osmotic controlled-release systems are a step up. A semi-permeable membrane surrounds an API-and-osmotic-agent core. Water seeps in at a fixed rate, dissolves the core, and pushes the drug solution out through a laser-drilled hole. Release kinetics approach zero-order and stay independent of pH and gastric motility. Clean engineering, but more expensive to manufacture.
Multi-layer tablets compress two or three different granulations into one unit. This handles combination products where APIs would degrade if blended, or biphasic release profiles where an immediate-release loading dose sits on top of an extended-release core. Bilayer presses with dual feed systems do the job.
Capsules get to modified release through pellets. The API goes onto sugar spheres or is extruded as pellets, then coated with release-controlling polymers at different thicknesses. The pellets are filled into the capsule shells. When the capsule dissolves, each pellet acts independently. This results in more predictable GI transit than a single monolithic tablet. But pellet manufacturing stacks up significant cost and complexity next to what a matrix tablet needs.
Quality Control and Inspection
Tablet QC checks more parameters than capsule QC. But capsule inspection is simpler because capsules have fewer mechanical failure modes.
Both forms get rigorous testing, but the test menus differ.
Tablet QC: weight variation per USP, hardness in kiloponds or Newtons (usually 4-10 kp), friability under 1.0% after tumbling, disintegration under 15-30 minutes, dissolution matching the spec, content uniformity across individual units, and visual inspection for chips, cracks, color spots, and foreign particles.
Capsule QC: weight variation, locking length (how much the cap overlaps the body after closure), disintegration with shell rupture under 15 minutes for gelatin, dissolution matching the spec, content uniformity, and visual inspection for dents, splits, incomplete closure, size variation, and print quality.
Inspection machines differ to match. A tablet capsule inspection system set up for tablets captures top, bottom, and side views. Capsule inspection needs fewer angles but has to measure the cap-body seam. If the seam isn’t right, the capsule fails. That’s a failure mode tablets don’t have.
| Parameter | Capsules | Tablets |
|---|
| Typical visual defect rate | 0.3-1.0% | 0.1-0.5% |
| Inspection machine speed | 50,000-100,000/hr | 80,000-150,000/hr |
| Most common defects | Dents, splits, improper closure | Chips, sticking, picking |
| Rejection mechanism | Compressed air | Compressed air or mechanical gate |
Choosing Between Capsules and Tablets: A Decision Framework

API characteristics and target patient population come first. Then production volume and available equipment. Cost comes third.
When you are deciding which form to go with, run through these questions in order:
- Is the API sensitive to moisture or oxygen? If yes, lean toward tablets with protective coating.
- Is the API very bitter or unpleasant? Capsules mask taste without extra processing.
- Does onset speed matter? Capsules dissolve faster than most tablets.
- Do you need modified release? Tablets give you more options. Multi-particulate capsules work well for some profiles too.
- What is your annual volume? Above 10 million units, tablet economics are hard to beat.
- What equipment do you already have? Matching an existing platform skips capital spending.
- Is the product going to high-humidity regions? Tablets handle tropical conditions without special packaging.
Many manufacturers run both lines. Tablet presses and capsule fillers are not mutually exclusive. Having both lets your formulation team pick the best delivery format per molecule instead of forcing everything onto one platform. A steady pipeline of empty capsules keeps improving with new polymer chemistries, and tablet presses keep getting faster with better weight control and containment for potent compounds.
Frequently Asked Questions
What are the main differences between hard gelatin capsules and soft gelatin capsules?
Hard gelatin capsules are two pre-formed interlocking pieces filled with dry material. Soft gelatin capsules are one-piece sealed shells made, filled, and sealed in a single continuous rotary die operation. Softgels usually carry liquid or semi-solid fills—oils, suspensions, and APIs with poor water solubility that benefit from lipid-based delivery. Hard capsules are more common in pharma because standard capsule filling equipment handles them with powder, pellets, or tablets.
Can a tablet press produce multi-layer tablets for combination products?
Yes. Bilayer and trilayer presses use separate feed systems to drop different granulations into the same die cavity in sequence. The first layer gets light pre-compression, the second layer goes on top, and the final compression bonds them together. This method handles combination drugs where the two APIs would degrade if blended or where immediate-release and extended-release layers share a single tablet.
How do enteric coatings on capsules differ from enteric coatings on tablets?
Enteric-coated capsules build gastric resistance into the shell itself—the shell gets treated with enteric polymers during manufacturing, or filled capsules go through a coating pan. Enteric-coated tablets apply the enteric polymer as a film over the compressed core. They work the same way: both survive stomach acid and dissolve in the small intestine’s higher pH. Which method to use comes down to whether you already have coating equipment and whether the capsule material can take the coating process conditions.