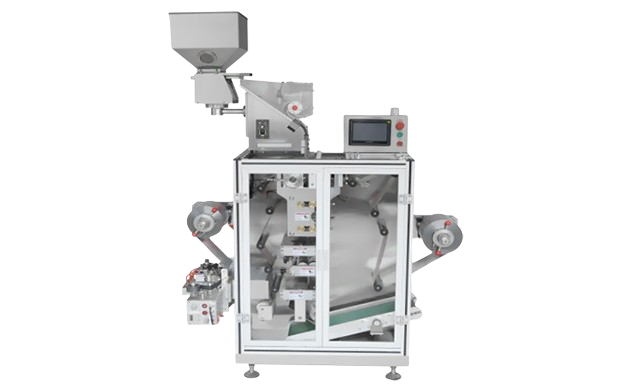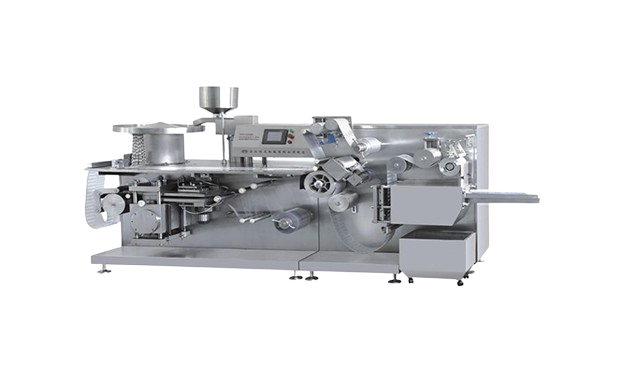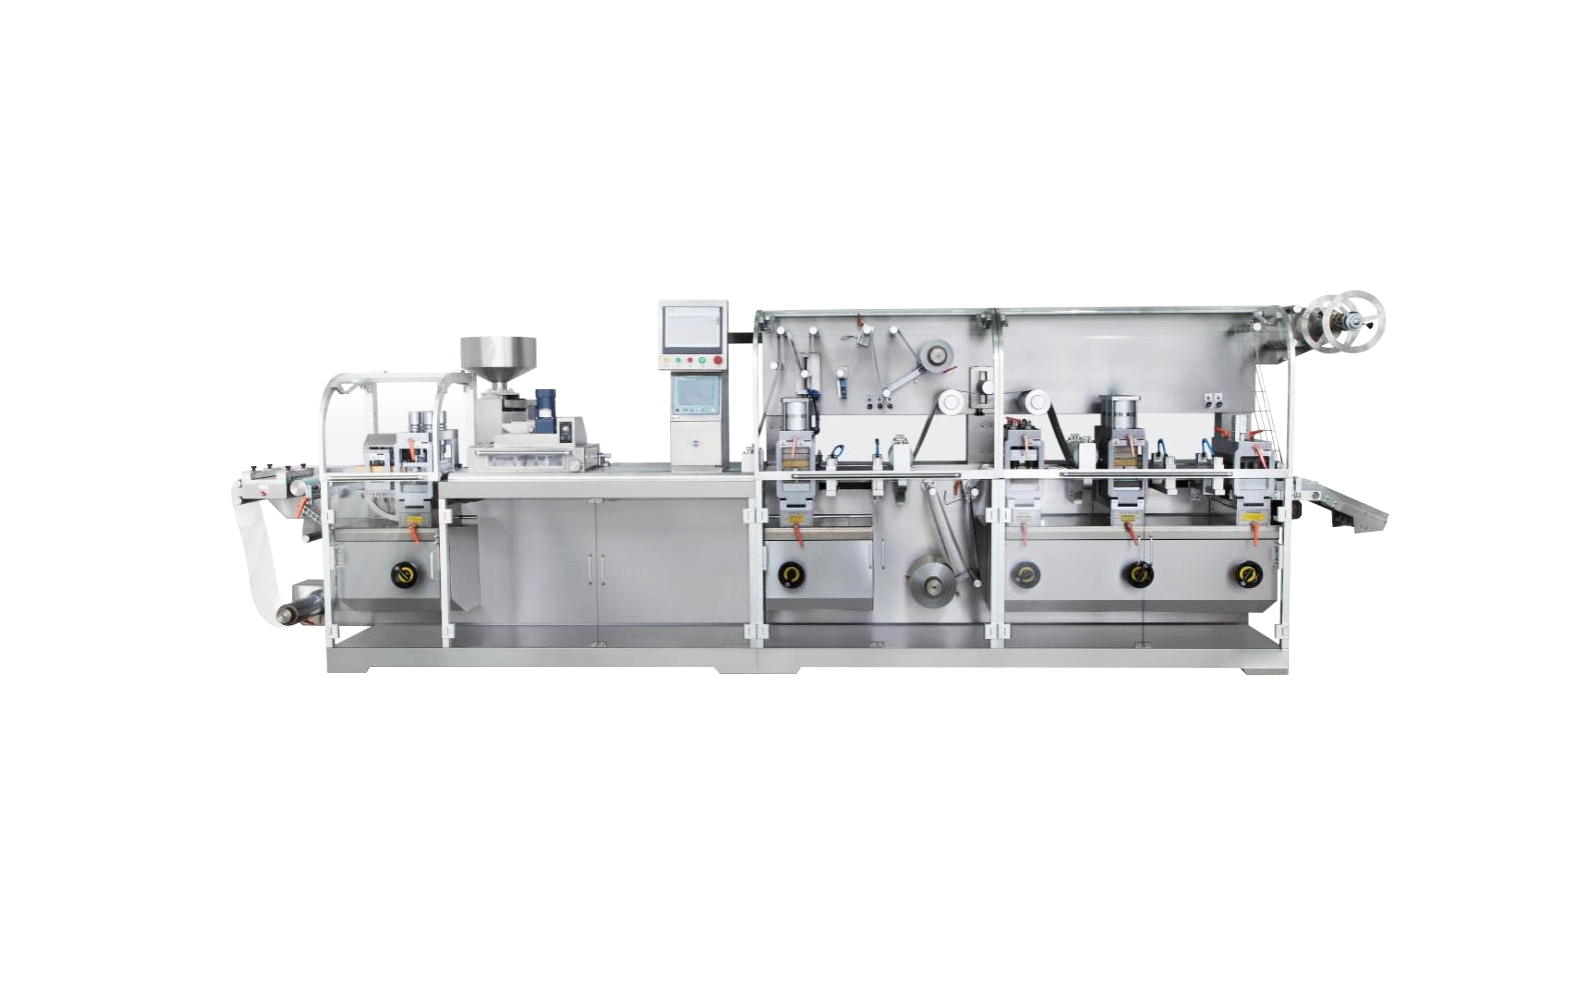
Buying pharmaceutical equipment one machine at a time can seem like the most flexible approach. You compare several quotations, select a supplier for each process, and build the line step by step.
On paper, that sounds reasonable. The difficulty usually appears when those machines need to work together.
A pharmaceutical production line is not simply a mixer, tablet press, capsule filler, inspection machine, and packaging machine placed in the same room. The capacity of one machine affects the next. Material needs to move between processes. Machine heights and discharge directions must match. Utilities, cleaning access, controls, inspection, and packaging all need to fit the same production plan.
A machine can work perfectly on its own and still create problems in the complete line.
This is why some manufacturers choose a one-stop pharmaceutical equipment solution. Instead of purchasing each machine as a separate project, one supplier or project team reviews the production process as a connected system.
The value is not just convenience. A well-planned one-stop solution can reduce capacity mismatches, simplify communication, identify layout problems earlier, and give the facility one main contact during installation and startup.
What Does a One-Stop Pharmaceutical Equipment Solution Actually Mean?
“One-stop solution” is used quite loosely in the equipment industry. Sometimes it simply means that a supplier sells several types of machines. That is not necessarily the same as providing a complete production solution.
A real one-stop project should begin with the product and process requirements. The supplier needs to understand what the facility will produce, how much it needs to produce, how the product will move through the line, and what happens after the main manufacturing process.
Depending on the project, the scope may include:
- Process and capacity planning
- Equipment selection
- Production-line layout
- Material-transfer planning
- Utility requirements
- Equipment connections
- Inspection and packaging integration
- Documentation
- Installation and commissioning
- Operator training
- Spare parts and technical support
Not every facility needs all of these services. A factory replacing one existing machine may only need a suitable model and help with installation. A new facility may need coordination from raw-material handling through final packaging.
The important point is clarity. The supplier should explain exactly what it will provide instead of using “turnkey” or “one-stop” as a general sales term.
The Complete Process Is Reviewed by One Team
When several suppliers are involved, each one naturally focuses on its own machine.
The granulator supplier looks at granulation. The tablet press supplier focuses on compression. The packaging supplier reviews the finished package.
The gaps often appear between those machines.
How will the granules reach the tablet press? Can the upstream process supply enough material? Will the tablets drop too far before entering the deduster? Can the inspection machine keep up? Is there enough space to remove tooling and clean the equipment?
These details may sound minor, but they can have a large effect on daily production.
With a one-stop solution, one project team can review the complete process before the equipment arrives. That team can look at the product route, machine arrangement, transfer points, expected output, and downstream requirements together.
For example, a solid-dose line may include material preparation, blending, granulation, tablet compression or capsule filling, polishing, inspection, counting or blister packaging, and cartoning. Each stage has its own requirements, but the stages still need to operate as one process.
The tablet manufacturing line guide and capsule production line guide explain those production routes in more detail. A one-stop project focuses on how the selected machines will support that route inside the actual facility.
Machine Capacities Can Be Matched More Realistically
One of the easiest mistakes to make is selecting every machine by its maximum speed.
A buyer may choose the fastest tablet press within the budget, then add a smaller inspection machine and a slower packaging line. The tablet press looks impressive in the quotation, but it may stop repeatedly because the downstream equipment cannot accept the output.
The opposite can also happen. A high-speed capsule filler may have plenty of capacity, but the material-preparation stage cannot supply powder consistently.
In both cases, the line is limited by something other than the main machine.
A one-stop supplier can compare the expected capacity of each stage and look for obvious bottlenecks before the equipment is ordered. This normally involves more than matching numbers in a catalog. The team should also consider material flow, product characteristics, cleaning time, changeovers, sampling, rejects, and normal production stops.
The goal is not to make every machine display the same rated output. Different equipment uses different units and runs under different conditions.
The more useful question is:
How many acceptable finished products can the complete line produce during normal operation?
In practice, a stable medium-speed line may produce more usable output than a poorly coordinated high-speed line.

Layout and Utility Problems Can Be Found Earlier
A machine may fit inside the room and still be difficult to use.
Operators need space to load material, remove tooling, clean product-contact parts, open electrical cabinets, and carry out maintenance. Conveyors and transfer containers also need room. Doors, columns, ceiling height, drains, personnel routes, and material routes can all affect the final layout.
This is where early planning matters.
When machines come from several suppliers, layout drawings and utility information may arrive at different times and in different formats. The facility team then has to combine everything and solve conflicts during construction or installation.
A one-stop supplier can prepare a coordinated equipment layout and utility list earlier in the project. The facility’s engineering team still needs to review and approve the final design, but it starts with a clearer picture.
The review should include:
| Area | Questions to confirm |
|---|---|
| Equipment space | Does each machine fit with enough operating and maintenance access? |
| Material flow | Can materials move between stages without unnecessary handling? |
| Personnel flow | Can operators work without crossing material routes? |
| Electrical supply | Do voltage, frequency, and power requirements match the facility? |
| Compressed air | Is enough pressure and flow available for all connected machines? |
| Dust control | Which processes need extraction or enclosed transfer? |
| Water and drainage | Are they required for cleaning, cooling, or processing? |
| HVAC | Can the room maintain the required production conditions? |
| Future expansion | Is there room for another machine, inspection unit, or packaging stage? |
It is not the most exciting part of an equipment purchase, but good layout planning can prevent a great deal of rework later.
Equipment Integration Becomes Easier to Manage
Two machines can operate correctly by themselves and still fail to work well together.
One machine may discharge at the wrong height. A conveyor may run in the wrong direction. The upstream machine may keep feeding after the downstream machine stops. A buffer may be missing between two processes. Control systems may use different signals.
These are not always serious engineering failures. Often, they are simply details that nobody owned during the purchasing stage.
A one-stop project team can review those connection points before installation. Depending on the level of automation, this may include:
- Transfer heights and discharge directions
- Conveyors and intermediate containers
- Start and stop signals
- Alarm communication
- Emergency-stop connections
- Product accumulation
- Line-speed coordination
- Inspection and rejection systems
- Data connections
The right level of integration depends on the facility.
A small-batch plant may prefer separate machines with manual transfer because this gives operators more flexibility. A high-volume facility may need automatic transfer and coordinated controls.
A good supplier should not automatically recommend the highest level of automation. It should recommend the level that makes sense for the product, production volume, labor plan, and budget.
Project Communication Has a Clearer Structure
Equipment projects generate a surprising number of questions.
Who confirms the conveyor height? Who provides the final utility list? Who changes the control signal? Who checks the line speed? Who is responsible when one machine stops another from running?
With several suppliers, these questions can move back and forth for days.
A one-stop solution gives the facility one main project contact. That person or team can coordinate the equipment package, collect technical information, and organize communication between the different machine groups.
This does not mean that every question receives an instant answer. Complex projects still require drawings, reviews, changes, and approvals. The difference is that responsibility is easier to follow.
Clear communication becomes especially important during installation. When a problem affects several stages, the project team can review the full process instead of checking one machine and saying that everything is working normally.
Documentation, Installation, and Training Are Easier to Coordinate
Pharmaceutical equipment projects usually involve much more than operating manuals. Depending on the facility, the document package may include equipment drawings, electrical and pneumatic diagrams, product-contact material information, spare-parts lists, FAT and SAT records, installation documents, training materials, and IQ/OQ support.
When machines come from several suppliers, these documents may arrive at different times and use different formats. The facility team then has to collect everything, confirm missing information, and make sure the documents match the actual equipment delivered. This work can take longer than expected, especially when one production line includes several connected machines.
A one-stop supplier can coordinate the document package across the project. This does not mean every document is automatically included. Before placing the order, confirm which documents the supplier will provide, which language they will use, and whether customized FAT, SAT, or qualification support is available. The agreed document list should appear clearly in the quotation or contract.
Installation is easier to manage when the same project team understands the full line. The team can coordinate equipment positioning, mechanical and electrical connections, line testing, trial production, and initial parameter adjustments. When a problem affects several machines, the supplier can review the full process instead of checking one machine in isolation.
For example, low tablet-line output may come from material preparation, compression, inspection, or packaging. Unstable capsule production may involve powder flow, filling settings, rejected products, or downstream bottlenecks. The tablet manufacturing line guide and capsule production line guide explain how these production stages connect.
Training can also follow the actual workflow rather than treating every machine as a separate subject. Operators need to understand startup, shutdown, cleaning, product changeovers, alarms, basic maintenance, and the effect one setting may have on the next machine. Increasing the speed of the main machine, for example, may overload the inspection or packaging section. A coordinated training plan helps operators understand the complete line and reduces unnecessary adjustments during normal production.

Future Products and Expansion Can Be Considered Earlier
Most pharmaceutical facilities do not produce the same product at the same volume forever. A factory may begin with one tablet size and later add coated tablets, capsules, new fill weights, or different packaging formats. Production demand may also increase as the product range grows.
When equipment is selected only for the first product, the line may become restrictive sooner than expected. A one-stop supplier can review both the current project and the manufacturer’s likely plans for the next two or three years. This may affect tooling ranges, product-contact parts, control systems, line layout, inspection options, packaging formats, and available utility capacity.
This does not mean buying the largest or most automated equipment available. Oversized machines can cost more, take up valuable floor space, and be inconvenient for small batches. The better approach is to select a practical starting configuration while leaving realistic room for new products or additional modules.
For example, the facility may not need an automatic inspection system during the first production stage, but it may be useful to reserve enough space and control connections for one later. SED Pharma’s automatic visual inspection machine range can be connected with tablet, capsule, bottle, and packaging processes when inspection requirements increase.
Thinking about future products early is usually less expensive than rebuilding the line after installation.
When Does a One-Stop Solution Make Sense?
A one-stop pharmaceutical equipment solution is especially useful for a new facility, a multi-machine production line, or a project that connects manufacturing, inspection, and packaging. It can also help when factory space is limited, the internal team has little experience with equipment integration, or the project needs coordinated documentation, installation, and training.
International projects may also benefit from this approach. Working with one main project team can reduce the number of suppliers involved in drawings, shipping, installation schedules, spare parts, and technical communication.
However, a one-stop solution is not necessary for every purchase. A single-machine order may be more practical when the existing line already works well, the facility only needs to replace one machine, or the internal engineering team can manage the connection work. A specialized machine from another supplier may also be the better choice when it meets a particular process requirement more effectively.
The purpose of a one-stop solution is to simplify a complex project. It should not make a straightforward equipment purchase more complicated.
SED Pharma’s pharmaceutical industry solutions cover equipment for dosage-form production, inspection, and packaging. The final project scope can include a complete line or only the machines the facility actually needs.
How to Evaluate a One-Stop Pharmaceutical Equipment Supplier
A large equipment catalog does not automatically mean that a supplier can manage a complete project. The supplier should be able to explain how it calculates line capacity, connects the machines, prepares the layout, manages documents, and supports installation.
Before making a decision, ask practical questions:
- Who will manage the complete project?
- How will the supplier calculate the actual line capacity?
- Which machines are produced directly, and which come from partners?
- How will the machines connect mechanically and electrically?
- What layout and utility information will be provided?
- Can the supplier test the equipment with the actual product?
- Which documents are included in the quotation?
- Who will manage installation and commissioning?
- What operator training is available?
- How will spare parts and technical support be handled?
- Can the line support future products or packaging formats?
- What is not included in the supplier’s scope?
The final question is easy to overlook, but it is often the most useful. A clear list of exclusions helps prevent misunderstandings about conveyors, utilities, cleanrooms, local installation work, validation, or secondary packaging equipment.
What Information Should You Give the Supplier?
A target speed alone is not enough to design a useful pharmaceutical production line. The supplier also needs to understand the product, process, factory, and final packaging requirements.
| Information | Details to provide |
|---|---|
| Product | Tablet, capsule, powder, liquid, cream, or another dosage form |
| Material | Flow, dust, moisture sensitivity, viscosity, or other relevant characteristics |
| Process | Main production stages and any process already confirmed |
| Product size | Tablet dimensions, capsule size, bottle size, or fill volume |
| Capacity | Batch size, hourly output, and annual production target |
| Packaging | Blister, bottle, sachet, carton, or another final format |
| Product range | Current products and possible future additions |
| Factory | Room dimensions, doors, ceiling height, and available layout drawings |
| Utilities | Voltage, frequency, compressed air, water, extraction, and HVAC |
| Automation | Manual transfer, semi-automatic operation, or integrated production |
| Inspection | Product, fill, count, seal, label, or code inspection |
| Documents | FAT, SAT, manuals, certificates, and qualification support |
| Schedule | Expected delivery, installation, and production-start dates |
It is also helpful to provide product samples whenever possible. Actual materials can reveal powder-flow, dust, static, breakage, feeding, filling, inspection, and packaging issues that are difficult to predict from specifications alone.
Do not send only a general message such as “we need a tablet line.” A supplier can prepare a more useful proposal when it knows the product size, formulation, process, output, packaging format, factory conditions, and documentation requirements.
Share these details through contact our team so the technical team can review the complete project rather than sending a general list of machines.
Frequently Asked Questions
Is a one-stop pharmaceutical equipment solution the same as a turnkey factory?
Not always. A one-stop equipment solution may include equipment selection, layout planning, line integration, documentation, installation, and training. A complete turnkey factory may also cover cleanrooms, utilities, building work, and other facility systems. The exact scope should be confirmed before ordering.
Is buying all the equipment from one supplier more expensive?
Not necessarily. Individual machine prices are only one part of the project cost. Integration work, modifications, installation delays, communication, training, downtime, and technical support should also be included in the comparison.
Can a one-stop line include machines from different manufacturers?
Yes. A project supplier may combine its own equipment with machines from specialist partners. The supplier should explain who produces each machine and who will be responsible for integration, documentation, and after-sales support.
Does a one-stop solution guarantee GMP compliance?
No. Equipment can support the facility’s requirements, but compliance also depends on factory design, operating procedures, qualification, validation, training, documentation, and daily production management.
Should we send product samples before ordering the equipment?
For many projects, product trials are highly valuable. Actual materials can reveal problems with flow, dust, static, breakage, feeding, filling, inspection, and packaging before the final equipment configuration is confirmed.
Conclusion
A one-stop pharmaceutical equipment solution is not simply a way to buy several machines from the same company. Its real value comes from planning the production line as one connected project.
When one team reviews equipment capacity, factory layout, machine connections, documentation, installation, training, and future expansion together, the project is usually easier to manage. It also becomes clearer who should respond when a problem affects more than one part of the line.
This approach makes the most sense for new facilities, multi-machine projects, and production lines that connect processing with inspection and packaging. For a simple replacement or upgrade, buying one suitable machine may still be the better option.
The goal is not to purchase the largest equipment package. It is to build a line that fits the product, factory, output, and future production plan.