The first time I walked through a pharmaceutical packaging facility, what stuck with me was how quiet everything was. Rows of blister lines cycling at 400 strokes per minute, and the loudest sound was the soft click of finished cards dropping into bins. Good blister packaging is boring in exactly the way you want pharma manufacturing to be.
The global blister packaging market crossed $22 billion in 2024. That number probably does not surprise anyone watching the shift over the last decade. More generics, more OTC products, more clinical trial materials. Everything is moving into blister formats. If you work in pharma production, procurement, packaging engineering, or quality, you will deal with blister packs.
A blister pack is pharmaceutical packaging made from a thermoformed plastic cavity that holds a single dose of medication, sealed on the back with a lidding material such as aluminum foil. Its job is to keep the drug away from air, moisture, light, and physical damage while giving the patient a unit dose they can push through without compromising the rest of the pack.
This guide covers how blister packs are built, the materials involved, the equipment needed to run a blister line, and the decisions that matter when choosing a format. I have organized it around the questions I get asked most by manufacturers setting up or upgrading their packaging operations.
What is a blister pack and how does it work
A blister pack forms a cavity in a plastic sheet, drops a tablet or capsule into it, and then heat-seals a backing material over the top. The result is an airtight seal around each dose that stays intact until someone forces the tablet through the foil.

The two layers
Every blister pack has two components. The forming film is the front side, usually PVC, PVDC-coated PVC, or PP, heated until soft and pulled into cavity shapes by vacuum or compressed air. The lidding foil is the back, typically aluminum foil with a heat-seal lacquer. Heat and pressure bond the lacquer to the forming film.
The drug sits between these layers. Push a tablet from the cavity side, and it breaks through the foil. The rest of the pack stays sealed. One dose, one breach. The principle has not changed in decades because it does not need to.
Step by step
A roll of plastic film feeds into the machine. First the heating station brings it to forming temperature. Then compressed air or vacuum shapes it into cavities. These cavities advance to filling, where tablets drop in through vibratory channels and capsules get oriented by tube feeders. The filled web meets the lidding foil at the sealing station, where heat and pressure bond the layers. A cutting station then punches the web into individual cards.
The materials that determine performance
PVC is cheap and thermoforms easily but is a terrible moisture barrier. Adding a PVDC coating cuts the moisture vapor transmission rate by a factor of 5 to 10. For seriously humidity-sensitive drugs, Aclar film pushes that improvement further. It is expensive but one of the best transparent barrier materials available.
Cold-form aluminum takes a different approach. Instead of thermoforming plastic, you stamp aluminum laminate at room temperature. The result is opaque and nearly impermeable. Cold-form provides the highest protection of any blister format but costs 30 to 50 percent more per unit and runs slower.
| Material | Moisture Barrier | Transparency | Relative Cost |
|---|
| PVC | Low | Clear | Lowest |
| PVC/PVDC | Medium | Clear | Low |
| Aclar | High | Clear | High |
| Cold-Form Alu | Very High | Opaque | Highest |
Key types of blister packaging in pharmaceuticals
Pharmaceutical blister packaging splits into thermoformed blisters made from heated plastic film and cold-form blisters stamped from aluminum laminate. The choice turns on moisture sensitivity, target shelf life, and budget.
Thermoformed blister packs
Thermoformed blisters account for most pharmaceutical blister volume. The cavities are transparent, so visual inspection of contents is built in. A rotary machine can form, fill, and seal over 600 blisters per minute. Basic PVC works for low-sensitivity drugs. PVC/PVDC covers the middle ground and is the workhorse of generic drug production. Aclar handles more demanding formulations.
Cold-form aluminum blister packs
Cold-form blisters use aluminum laminate for both the cavity and the lidding. A press stamps the material at room temperature. The cavities are thicker, and the package is completely opaque. These are the defaults for drugs that degrade rapidly with moisture: proton pump inhibitors, certain antibiotics, and dry powder inhaler formulations. You cannot push through cold-formed. These packs need peel-off lidding or a tear notch.
Blister card packaging
Blister card packaging attaches a thermoformed blister to a printed cardboard backing that carries branding, dosing instructions, and regulatory text. This format dominates OTC retail. The card stock needs to be stiff enough to hold the blister securely but not so thick it jams the tooling. Blister card packaging covers the full set of design tradeoffs.
Strip packaging
Strip packaging seals individual doses between two layers of flexible foil laminate with no formed cavities. Each dose sits flat between layers and tears off at perforations. Strip packs handle effervescent tablets and single-dose powders well because there is no cavity geometry to match. The downside: slower production and patients find them harder to open than push-through blisters—which matters for elderly users.
How blister packs compare to other formats
Blister packs provide stronger unit-dose protection and built-in tamper evidence than bottles but cost more per unit and need specialized equipment. The right format depends on the drug, production volume, and the climate where the product will be sold.

The bottle versus blister tradeoff
Bottles win on cost and simplicity. A bottle filling line costs less to buy and run. The economics are hard to argue with for high-volume generics.
The problem is what happens after opening. Every tablet inside gets exposed to ambient air. In a humid bathroom in Southeast Asia, a bottle of aspirin can absorb enough moisture in weeks to start degrading. Blister packs avoid this by design. Each cavity is its own micro-environment. Opening cavity three does nothing to cavity four. For drugs shipping to ICH Zone IV countries, this stability advantage often outweighs the higher packaging cost. The Blister Packaging in the Pharmaceutical Industry guide covers format selection in more detail.
Cost comparison at scale
| Factor | Blister Pack | Bottle | Strip Pack |
|---|
| Per-unit cost | Medium | Low | Medium-High |
| Moisture protection after first use | Full | None | Full |
| Tamper evidence | Built into design | Needs separate seal | Built into design |
| Patient adherence support | Calendar blisters work well | Minimal | Moderate |
| Production speed | 200 to 600/min | 100 to 300/min | 150 to 400/min |
| Changeover time | 30 to 90 min | 10 to 30 min | 20 to 60 min |
Where blister packs make the most sense
Unit-dose dispensing in hospitals is a blister-only world. Nurses grab a single dose, administer it, and document it. Bottles do not fit that workflow. Clinical trial packaging works the same way: blinded studies need precise dose control and tamper evidence for every administration. Calendar blister packs also improve adherence in elderly patients by 15 to 25 percent compared to bottles.
Equipment needed for blister packaging production
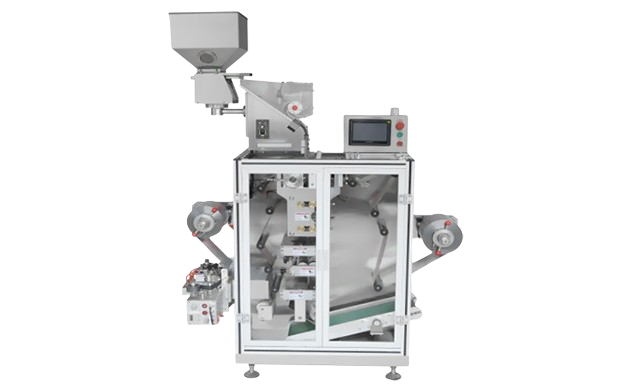
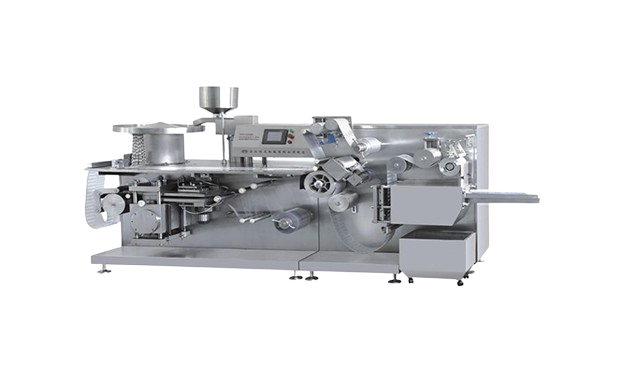
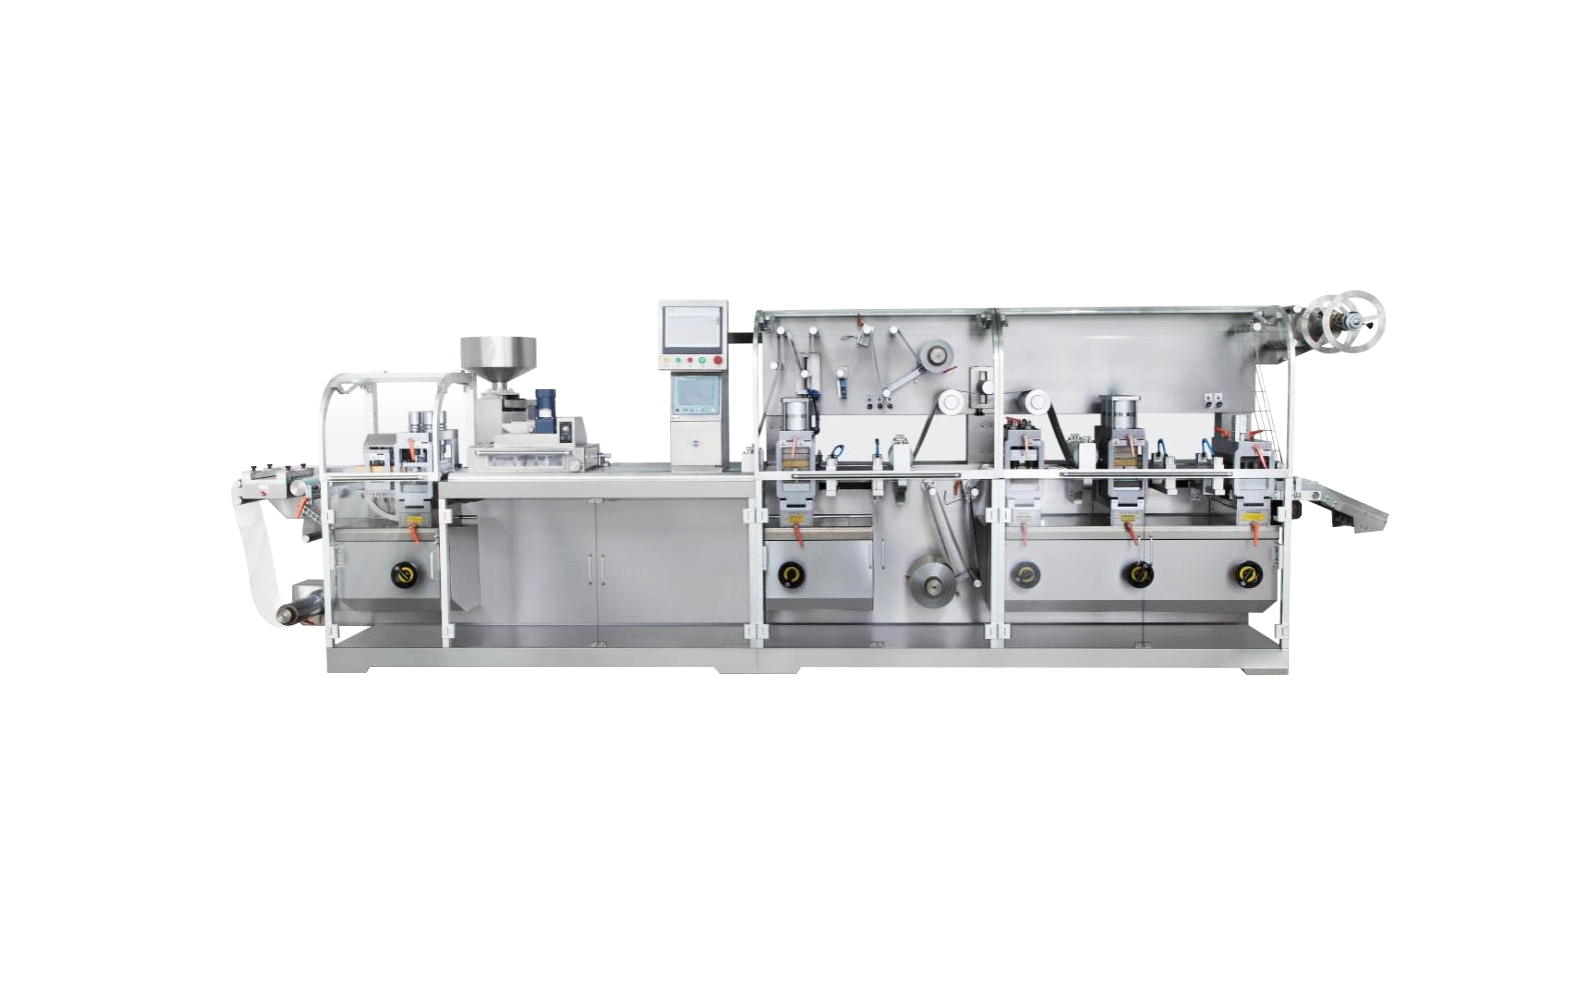
A blister packaging line centers on a forming and sealing machine, supported by product feeding, inspection, and downstream modules for cartoning and serialization. The machine type determines your speed ceiling, material flexibility, and changeover economics.
Choosing a blister machine
Rotary machines run the fastest at 500 to 600 blisters per minute on a continuously rotating drum. The catch is material flexibility. Rotary machines do not handle cold-form aluminum well.
Flat-plate machines use intermittent motion. The film indexes, stops, gets formed and sealed, and then indexes again. Slower than rotary but far more flexible. You can run PVC, PVDC, Aclar, and cold-form on the same machine. Most mid-volume lines use flat-plate architecture.
Platen-sealing machines are simpler and suit small batches, R&D, and clinical trial packaging where speed matters less than quick changeover.
Feeding and inspection
Vibratory feeders work for round tablets and firm gelatin capsules. Brush boxes sweep excess product while gently pressing tablets into cavities. For softgels, tube feeders with cushioned drop surfaces reduce breakage.
After sealing, every blister needs inspection. Missing tablets, broken tablets, foil wrinkles, and incomplete seals. Manual inspection works up to maybe 30 per minute. At 300 per minute, you need automation. Tablet Capsule Vision Inspection Machine systems use multiple cameras and LED lighting to catch defects that human inspectors miss. Reject stations downstream blow defective blisters off the line.
Downstream modules
A cartoning machine erects cartons and inserts blister cards. A checkweigher verifies contents by weight. A serialization module applies unique identifiers for track-and-trace. A bundler and case packer finish the line. The whole system runs at the speed of its slowest module. A bottleneck at the cartoner can cut effective output by 30 percent even if the blister machine runs at full speed.
Quality control and regulatory considerations

Blister packs must meet pharmacopeial standards for seal integrity, moisture barrier, and material safety. QC during production involves leak testing, peel strength testing, and visual inspection at defined sampling intervals.
The tests that matter
Blue dye immersion is the most common leak test. Submerge samples in methylene blue under vacuum. If dye enters a cavity, the seal has failed. Cheap and visual, but destructive and qualitative.
Vacuum decay testing is quantitative and non-destructive. Place a blister in a sealed chamber, pull vacuum, and measure the pressure rise rate. A leaking blister releases air. Slower and costlier than blue dye, but the data supports trending and process control.
Peel strength testing measures the force to separate lidding from forming film. The sweet spot for push-through blisters is 4 to 8 newtons of peel force. Too weak and the blister fails during transport. Too strong, and elderly patients cannot push through.
Dimensional checks verify cavity depth, wall thickness, and card dimensions. Print registration checks confirm lot numbers, expiry dates, and barcodes are legible. Sampling plans follow AQL 1.0 or 0.65 depending on the risk assessment.
Regulations across markets
The FDA expects container-closure integrity testing under 21 CFR 211.166. The EU’s Falsified Medicines Directive requires unique identifiers and tamper-evident features on prescription drug packaging. The WHO publishes guidelines adopted by many emerging markets. Some require child-resistant formats for certain drug classes. Some require braille on lidding foil. A design that works for the US may need changes for Brazil or Saudi Arabia.
Common defects and root causes
Incomplete seals usually trace to sealing temperature or pressure being too low, dwell time too short, or contamination on the sealing surface. Sometimes the root cause is a worn forming tool producing inconsistent cavity rim thickness.
Deformed cavities come from forming temperature drift or uneven heating. Foil cracking comes from material defects, excessive web tension, or worn cutting tools. The best operators do not guess. They read the machine. They check temperature profiles every hour whether the line is running well or not.
Where blister packaging is heading
The blister packaging industry is being pushed toward recyclable materials, packaging with digital health features, and production lines with less human intervention. Each direction brings its own engineering challenges.
The sustainability problem
PVC blister packs are hard to recycle because PVC and aluminum must be separated. Europe is pushing hard on packaging waste regulation, and pharma companies have announced packaging sustainability targets.
Suppliers have responded with mono-material PP blisters compatible with polyolefin recycling streams and PET blister films with high-barrier coatings. The problem is barrier performance. PP and PET without coatings do not match PVDC-coated PVC, let alone Aclar or cold-form aluminum. Coatings that improve barrier performance also complicate recycling. Getting both sustainability and a high barrier in one package is still an active area of R&D.
Smart features and serialization
NFC tags embedded in blister cards let patients scan packaging to verify authenticity and access dosing instructions. Printed electronics can detect when a tablet is pushed out and log the timestamp, valuable for directly observed therapy programs like tuberculosis treatment.
Serialization is expanding beyond the EU. The US DSCSA, Russia’s Chestny ZNAK, and similar programs in Turkey, Saudi Arabia, and South Korea all require unique identifiers. Manufacturers are integrating pharmaceutical packaging design workflows with printing, vision verification, and serialization directly on the line.
Automation on the production floor
Blister lines are being connected to manufacturing execution systems that log temperature, pressure, reject counts, and line speed in real time. Predictive maintenance pulls vibration data from sealing station bearings. When the signature shifts in a pattern that preceded a failure on a previous run, the system flags it before the bearing fails.
Some facilities run lights-out production for entire shifts. Blister machine, cartoner, case packer — nobody on the floor. AGVs deliver film rolls and take away pallets. Expensive to set up and harder to validate, but facilities that have done it report 15 to 25 percent per-unit cost reduction over the equipment lifecycle. The bigger benefit is consistency: every seal sees the same parameters, and the data trail is complete.
FAQ
What is the difference between a blister pack and a strip pack?
A blister pack has a formed cavity giving it a 3D bubble shape. A strip pack seals the product flat between two flexible layers. Blister packs let patients push tablets through foil. Strip packs tear open at perforations. Strip packs handle powders and effervescent tablets better. Blister packs are faster and cheaper per unit at volume.
How long do tablets last in blister packaging?
Tablets in high-barrier packs like Aclar or cold-form aluminum stay stable for 2 to 5 years under proper storage. Shelf life depends on the drug formulation, the barrier properties of the film combination, and storage temperature. Products in basic PVC blisters get shorter shelf lives.
Can blister packs be recycled?
Standard PVC and aluminum blisters are difficult to recycle because the layers must be separated. The industry is moving toward mono-material PP blister packs compatible with polyolefin recycling. Some manufacturers run take-back programs through specialized facilities that recover both plastic and aluminum fractions.