Size 0 is the workhorse capsule size of the pharmaceutical and supplement industries. It holds enough powder for most adult doses, it is easy to swallow, and almost every capsule filling machine on the market is built around it. But “compatible with size 0” and “fills size 0 well at production scale” are two different things. Buyers who choose a machine on price alone often discover the difference through weight variation, cracked shells, and rejected batches.
The best capsule filling machine for size 0 capsules depends on your daily output, your powder characteristics, and your budget. For batches under 50,000 capsules per day, a semi-automatic machine is usually the most cost-effective choice. For continuous production above 100,000 capsules per day, a fully automatic machine delivers the accuracy and labor savings that justify its price. The sections below walk through the specifications, the dosing challenges, and the selection criteria so you can match a machine to your actual production needs.
Here is a quick comparison before we go into detail.
| Machine type | Output (capsules/hour) | Labor needed | Fill accuracy | Best for |
| Manual filler | 100–800 | High, fully manual | Operator-dependent | R&D, pilot batches |
| Semi-automatic | 6,000–35,000 | One trained operator | Good, ±3–5% typical | Small- to mid-size plants |
| Fully automatic | 25,000–200,000+ | Minimal, supervisory | High, ±1–3% typical | GMP mass production |
Specifications are subject to the technical data sheet for the specific model and test results using the customer’s materials; please note that powder flow ability, capsule shells, and operating speed will affect the results.
Size 0 capsule specifications and why they matter for machine selection

A size 0 capsule has an internal volume of about 0.68 mL, a locked length of roughly 21.7 mm, and an outer diameter of about 7.6 mm at the cap, with the body measuring about 7.34 mm. These are the dimensions published in the size chart of a major hard capsule shell supplier, which you can check on this two-piece hard capsule size chart; that chart prints a tolerance of ±0.3 mm on closed length. The numbers look simple, but they define the tooling, the dosing depth, and the locking force your machine must deliver.
Size 0 sits in the middle of the standard capsule range, which runs from 000 (the largest) down to 5 (the smallest). You can see where it falls on a full capsule size chart. Because it balances capacity and swallowability, it is the default size for vitamins, herbal blends, probiotics, and many prescription and OTC drugs. That popularity has a practical consequence for buyers: most machines are engineered and tested around size 0 first, so tooling availability and spare parts are rarely a problem for this size.
One caution before you set up tooling: shell suppliers do not publish identical figures for every size. Published values for size 0 vary slightly between suppliers and between gelatin and HPMC shells, so the data sheet for the shells you actually buy is the document your tooling should be machined against, not a generic table.
The specifications still set hard requirements for the equipment:
- Separation rings and segment plates must match the 7.34 mm body diameter closely. Poorly machined segments cause split shells and capsules that fail to separate.
- Dosing depth must be calibrated to the 0.68 mL volume. Shallow dosing wastes capsule capacity; deep dosing overcompresses the powder plug and can deform the body.
- Locking pins must apply enough force to close a 21.7 mm capsule without denting it.
This is why two machines that both “support size 0” can produce very different results. The specification support is in the tooling quality, not in the brochure.
How much powder fits in a size 0 capsule?
A size 0 capsule has no fixed fill weight. Its volume is fixed at 0.68 mL; the weight depends on the bulk density of your material. Run that fixed volume across the density range most powders occupy and you get a calculated span of roughly 270 to 820 mg. Treat that span as an arithmetic illustration, not as a fill specification or a guaranteed capacity for your product.
The relationship is straightforward:
Fill weight (mg) = Volume (mL) × bulk density (g/mL) × 1000
Example only. Every figure below is the result of that formula at a 0.68 mL volume, shown to illustrate the relationship. None of them is a specification, a maximum, or a target for your formulation.
| Powder bulk density | Calculated fill weight (0.68 mL × density) |
|---|---|
| 0.4 g/mL (light, fluffy botanicals) | ~272 mg (below the range most supplier charts publish) |
| 0.6 g/mL (average herbal blend) | ~408 mg |
| 0.8 g/mL (typical granulated blend) | ~544 mg |
| 1.0 g/mL (dense mineral powder) | ~680 mg |
| 1.2 g/mL (very dense material) | ~816 mg |
Most supplier size charts publish the 0.6 to 1.2 g/mL rows only, so the 0.4 g/mL line above is an extrapolation using the same formula. In practice, no dosing system fills 100% of the geometric volume, and the achievable figure also depends on how well your powder flows and compresses. The only number that should reach a purchase order is the one measured on a trial fill with your own powder and your own shells.
Two details matter for production planning. First, machines fill by volume, so any fluctuation in your powder density shows up directly as fill weight variation. Second, you should target 80–90% of the capsule’s capacity, not 100%. A fully packed capsule leaves no head space for normal process variation and is more likely to fail at the locking station.
Weight variation is not just a quality issue; it is a regulatory one. USP <905> Uniformity of Dosage Units is the harmonized general chapter that sets the acceptance logic most regulators follow. It does not name a single fixed percentage for fill weight; it defines an acceptance value calculated from the mean, the standard deviation, and the sample size, with the maximum allowed acceptance value set at 15. Your fill weight control strategy has to keep every capsule inside those limits. This is also why experienced buyers send their actual powder for a trial fill before purchasing: the density you measure in the lab is the number that determines dosing disc selection and tamping settings, not a value from a reference table.
What makes filling size 0 capsules difficult at production scale?
The main difficulties are fill weight consistency, capsule damage, powder behavior, and changeover downtime. All four get worse as speed increases.
At 400 capsules per hour, an operator can catch problems by eye. At 40,000 capsules per hour, a small misalignment becomes thousands of rejected capsules before anyone notices. The specific pain points for size 0 production include:
- Fill weight drift. Fine or poorly flowing powders do not feed evenly into the dosing disc cavities. The result is a weight spread that grows wider as the hopper empties or as humidity changes the powder’s flow.
- Capsule separation failures. Size 0 shells are thin. If vacuum or mechanical separation is mistimed, bodies crack or caps stay attached, and fragments end up in the dosing station.
- Dust and cross-contamination. Light powders escape during tamping and settle on the segment plates, causing misalignment in later stations.
- Changeover losses. A plant running size 0 in the morning and size 1 in the afternoon loses production time every time the tooling swap is slow or imprecise.
Low-cost machines concentrate their weaknesses exactly here: soft segment plate tolerances, inconsistent tamping pressure, and dosing discs that wear quickly. The purchase price looks attractive until you calculate the cost of rejected capsules and unplanned stops over a year of production.
How a capsule filling machine handles size 0 capsules

A capsule filling machine processes size 0 capsules through a fixed sequence of stations: orientation, separation, dosing, rejection, locking, and discharge. Each station has tooling machined specifically for the capsule size.
- Orientation and loading. Empty capsules drop from a hopper into segment plates, aligned body-down.
- Separation. Vacuum or mechanical fingers pull the caps from the bodies. The caps stay in the upper segment; the bodies drop into the lower segment for filling.
- Dosing. Powder is measured into the capsule body, either by a dosing disc with tamping pins or by a dosator tube.
- Rejection. Faulty capsules — unseparated, cracked, or misaligned — are detected and ejected before locking.
- Locking. The upper and lower segments realign, and pins press the cap onto the body until the locking ring clicks shut.
- Discharge and cleaning. Finished capsules exit the machine, and compressed air clears the stations for the next cycle.
Tamping pin vs. doser dosing for size 0
The two mainstream dosing systems behave differently with size 0 capsules:
- Tamping pin (dosing disc) systems compress the powder into a plug in stages, using five or more tamping stations, then transfer the plug into the capsule body. They handle a wide range of powder densities and are the standard choice for high-speed automatic machines. For size 0, the disc thickness and pin stroke are set to the 0.68 mL target volume.
- Dosator systems suck powder into a tube, compress it with a piston, and push it into the body. They handle low-dose and low-fill applications well and are gentler on fragile granules, but they are more sensitive to powder flow ability.
For most size 0 supplements and generic drug production, tamping pin dosing offers the better combination of speed and weight consistency. Dosator systems earn their place when the dose is small relative to capsule capacity or when the formulation is abrasive.
Manual vs semi-automatic vs automatic capsule filling machine for size 0
For size 0 production, the choice comes down to daily volume: manual fillers suit lab-scale work, semi-automatic machines suit small and mid-size plants, and fully automatic machines suit continuous GMP production. Specifications are subject to the technical data sheet for the specific model and test results using the customer’s materials; please note that powder flow ability, capsule shells, and operating speed will affect the results.
| Factor | Manual | Semi-automatic | Fully automatic |
| Output for size 0 | 100–800/hour | 6,000–35,000/hour | 25,000–200,000+/hour |
| Operators required | 1–2, constant work | 1, with tray handling | 1 supervisor per line |
| Fill weight accuracy | Operator-dependent | ±3–5% | ±1–3% |
| Tooling changeover | Minutes | 30–60 minutes | 1–2 hours, size-dependent |
| Typical price range | Very low | Mid | High, lowest cost per capsule at scale |
| GMP fit | Limited | Yes, with procedure control | Yes, designed for it |
A practical rule of thumb: if your size 0 output stays below 50,000 capsules per day, a semi-automatic capsule filling machine covers the volume at a fraction of the automatic price, and its simpler structure keeps maintenance in-house. Once daily demand passes roughly 100,000 capsules, the labor cost and weight-variation losses of semi-automatic production overtake the price gap, and a fully automatic machine becomes the cheaper option per capsule.
Also check multi-size capability before you buy. Most quality machines fill sizes 000 through 5 with a tooling change, so a machine bought for size 0 today can run size 1 or 00 tomorrow without a new capital purchase.
How to choose the right model: a buyer’s checklist

The right model is the one that meets your output target with documented accuracy, GMP-compliant contact parts, and support you can actually reach. Evaluate every candidate against the same checklist:
- Rated output for size 0 specifically, not a theoretical maximum for the easiest size.
- Fill weight accuracy stated as a percentage with a test method behind it.
- Contact part materials: 316L stainless steel for powder contact, with surface finish documentation.
- Rejection and inspection functions: unseparated capsule detection, empty capsule rejection, and optional weight checking.
- Changeover time and tooling cost for the sizes you plan to run.
- Compliance documentation: CE marking and a design that supports your CGMP obligations.
- After-sales structure: spare parts stock, response time, and remote support capability.
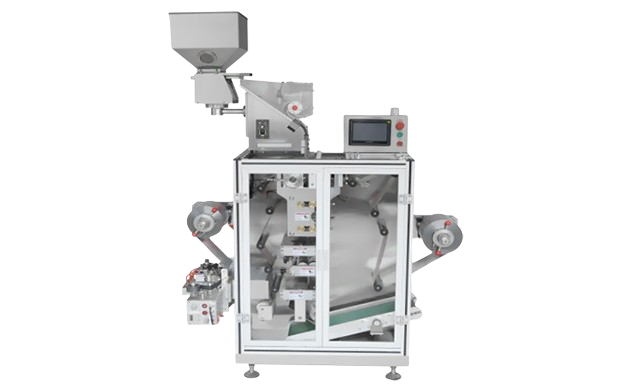
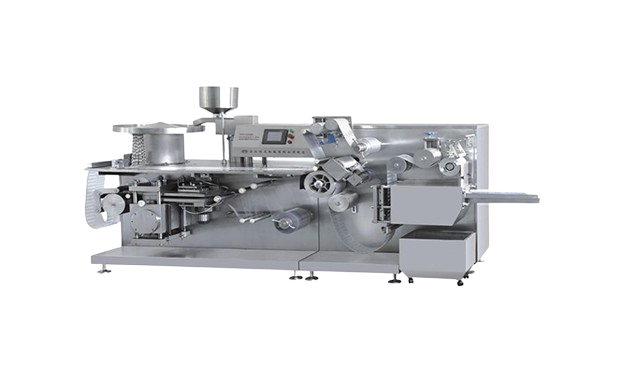
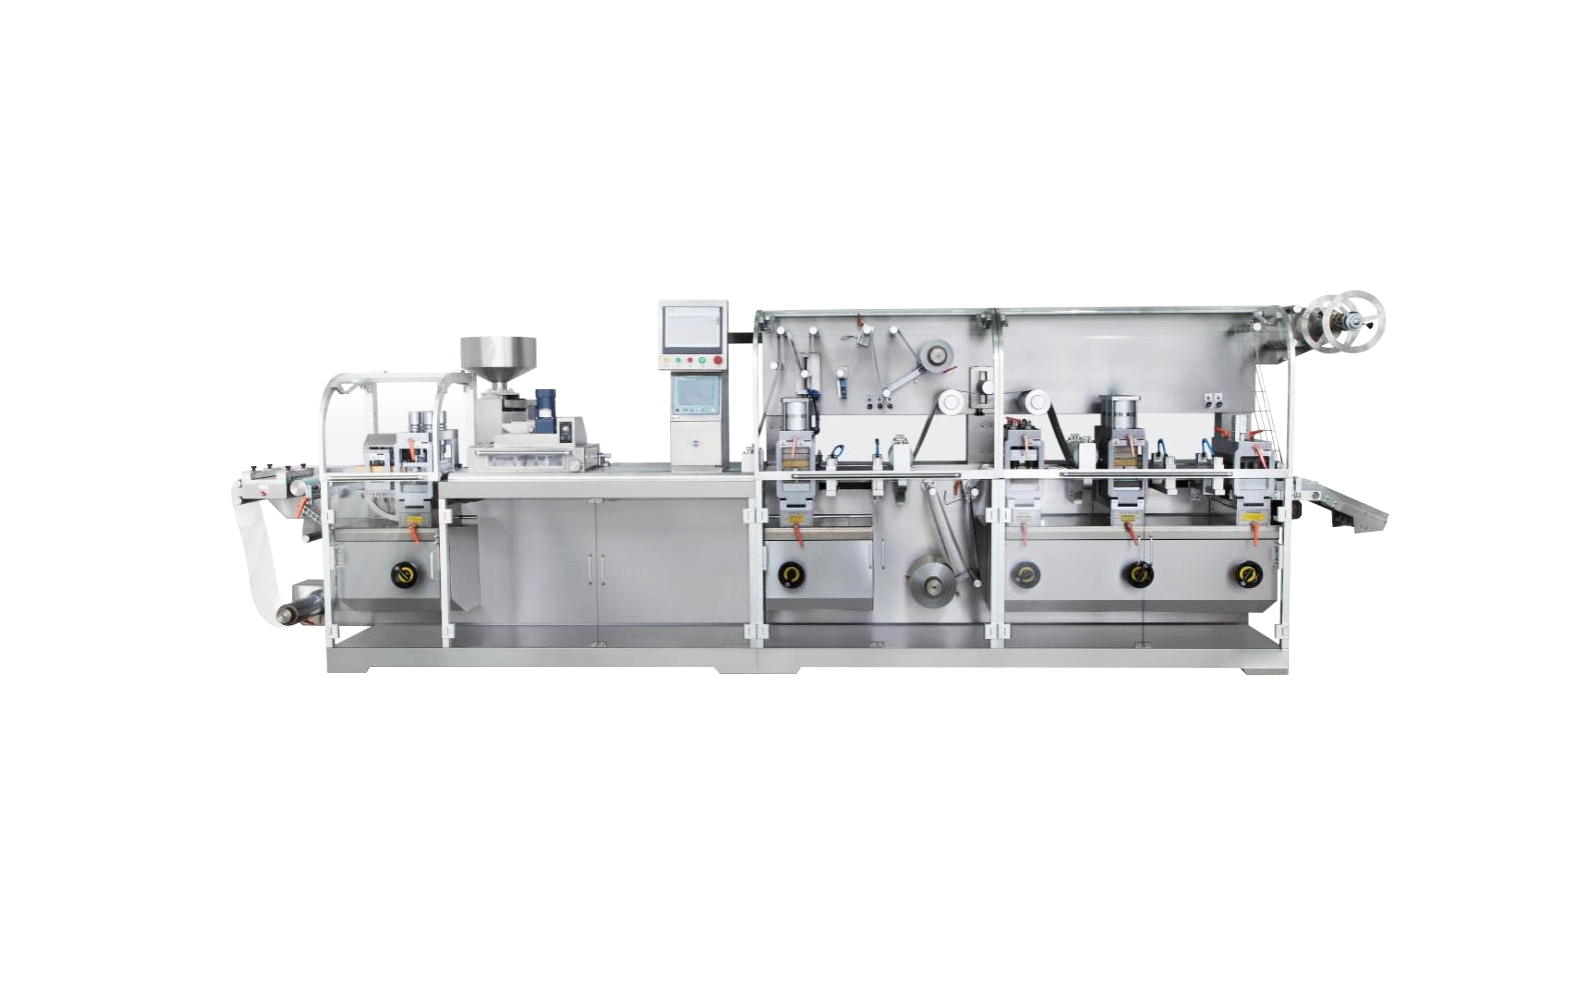
SED Pharma builds both tiers of this decision, and the numbers differ model by model rather than by series. The semi-automatic SED-BJ series runs 10,000–40,000 capsules per hour across capsule sizes 000# to 5#, with adjustable filling volume and speed for plants that switch between formulas. On the automatic side, the SED-J-H covers 12,000–228,000 capsules per hour in sizes 00# to 4#, while the SED-J-I spans 7,200–450,000 capsules per hour in sizes 00# to 5#. Both platforms run the full cycle from capsule loading through waste rejection and finished product discharge, use mold changes to move between sizes, and are built for continuous pharmaceutical and nutraceutical production. Both lines use precision mechanical and pneumatic dosing with sensor-based controls, and both ship with the documentation packages buyers need for validation.
If you share your target daily output and powder details, the SED engineering team can recommend a specific configuration rather than a generic model number.
Sample testing and trial run requirements before purchase
A trial fill with your actual powder and your actual capsule shells is the single most reliable way to de-risk the purchase. Reputable manufacturers expect this request and have a process for it.
A typical sample test requires the following:
- Powder sample: a sufficient quantity of the production blend, enough to run sustained filling rather than a few token capsules.
- Empty capsule shells: a supply of the exact size 0 shells you plan to buy, because gelatin and HPMC shells behave differently on the machine.
- Test protocol: agreed acceptance criteria for fill weight variation, separation success rate, locking quality, and capsule damage rate.
- Report: documented results with weights, speeds, and rejection counts.
A trial fill with your actual powder and capsule shells is the single most reliable way to de-risk the purchase. Reputable manufacturers expect this request and have a process for it. The required sample quantity, acceptance criteria, and deliverables are confirmed by the engineering team based on the specific powder characteristics and machine model.
Integrating the filler into a complete capsule production line
The filling machine is the center of the line, but it does not work alone. Upstream, your powder comes from mixing and possibly granulation or milling equipment; downstream, filled capsules need polishing, weight checking, inspection, and packaging.
A complete capsule production line for size 0 typically flows like this:
- Powder preparation: milling, mixing, and granulation as required
- Capsule filling
- Capsule polishing to remove surface dust
- Checkweighing to reject out-of-tolerance capsules
- Visual or metal inspection where required
- Counting and bottling, or blister packaging
Planning the filler and the line together avoids the classic mismatches: a filler that outruns the polisher, a checkweigher that cannot keep up with line speed, or a packaging inlet at the wrong height. SED Pharma supplies the filling, polishing, counting, and packaging equipment as a matched set, with interface dimensions confirmed during layout design, so the line runs as one system instead of a collection of separate purchases.
Get a quotation: what information to prepare
A useful quotation comes from specific production data, not from a price list. When you contact a manufacturer, prepare the following so the recommendation matches your plant:
- Target output: capsules per hour or per day, for size 0 and any other sizes you plan to run
- Powder information: bulk density, flow ability, moisture sensitivity, and whether the blend is granulated
- Capsule shells: gelatin or HPMC, and your intended supplier if known
- Plant conditions: available floor space, power supply, compressed air, and cleanroom grade
- Budget range and timeline: including whether you need a single machine or a full line with polishing, counting, and packaging
SED Pharma’s engineering team uses exactly this checklist to configure proposals, and trial testing with your own material can be arranged before you commit. Send your production requirements through the inquiry form on the site, and you will receive a machine recommendation, a layout suggestion, and a quotation based on your actual filling task rather than a generic catalog page.
The bottom line on size 0 capsule filling
Size 0 is the industry default because it is forgiving, not because it is easy to run well. The dimensions are fixed, but the results depend on whether the tooling is machined to them, whether the dosing depth matches your powder’s bulk density, and whether the machine holds that accuracy at the speed you actually need.
Three points decide most purchases:
Daily output. Below roughly 50,000 capsules a day, a semi-automatic machine covers demand at a much lower capital cost. Above about 100,000, labor and reject savings make an automatic machine cheaper per capsule.
Powder behavior. Machines dose by volume, so density swings, poor flow, and humidity show up as weight variation. A trial fill on your own blend is the only way to see it before you buy.
Tooling and service. Segment plates, dosing discs, and locking pins are wear parts. Spare stock and a reachable service team matter more over five years than a small difference between two quotes.
A brochure tells you whether a machine claims size 0. A trial run on your powder and your shells tells you how it fills it. If you are still weighing the two tiers, work out the output you need on an average day and send it with your powder data. SED Pharma’s engineers match configurations across the capsule filler range, arrange trial filling with your material, and return a quotation built around that production task. Specifications are subject to the technical data sheet for the specific model and test results using the customer’s materials; powder flow ability, capsule shells, and operating speed will affect the results.
Send your target output, powder details, and plant conditions through the contact us page, and you will get a specific model recommendation and a layout suggestion rather than a generic catalog page.
FAQ
What fill weight variation is acceptable for size 0 capsules?
There is no single universal number, because the limit depends on your product and market, but the pharmacopoeial framework set out in USP <905> is the acceptance logic most regulators follow. In practice, well-maintained automatic machines hold ±1–3% on size 0, and semi-automatic machines hold ±3–5%. If your measured variation drifts wider, the cause is usually powder flow, worn tooling, or incorrect tamping settings rather than the capsule size itself. Specifications are subject to the technical data sheet for the specific model and test results using the customer’s materials; please note that powder flow ability, capsule shells, and operating speed will affect the results.
Do HPMC capsules run differently from gelatin capsules on the same machine?
Yes, and the difference matters at production speed. HPMC shells are slightly less elastic than gelatin, so they need gentler separation force and careful humidity control in the filling room, typically 35–55% relative humidity. Most quality machines run both materials on the same tooling with adjusted settings, but you should confirm this in the trial run with the exact shells you intend to buy.
When should a plant upgrade from semi-automatic to fully automatic?
The trigger is usually economic rather than technical. When daily size 0 demand passes roughly 100,000 capsules, the extra labor, the wider weight variation, and the per-capsule material waste of semi-automatic production typically cost more per year than the loan or lease on an automatic machine. Plants approaching that volume, or facing a compliance audit that demands tighter process control, should start the evaluation before the bottleneck arrives.