Introduction
Why does blister packaging matter in the pharmaceutical industry? Since in addition to being a form of packaging, it also brings unique value to the pharmaceutical industry, which is reflected in the protection, quantification, safety, shelf life and other needs of medicines.
In the highly regulated pharmaceutical industry, packaging serves as the final yet critical line of defense in ensuring drug efficacy, patient safety, and regulatory compliance. Among the various packaging solutions available, blister packaging has emerged as the gold standard for solid oral dosage forms, accounting for over 70% of unit-dose packaging in developed markets (Pharma Packaging Trends Report, 2023).
Blister packing consists of a thermoformed plastic cavity (usually PVC, PVDC or cyclic olefin polymer) sealed with an aluminum foil or paper cover. This packaging format has advantages in terms of moisture barrier performance, dosage control and patient compliance mechanisms. This article mainly covers:
- Which specific pill form categories can benefit most from blister packaging
- Detailed technical comparison with other packaging formats
- Choosing a best blister packing machine manufacturer that meets your needs
What Pill Types Are Benefit from Blister Packs?
Hygroscopic and Moisture-Sensitive Formulations

Blister packaging provides critical protection for drugs susceptible to hydrolysis:
- Antibiotics (amoxicillin, doxycycline): With its moisture-proof properties, aluminum-plastic blister packaging can strictly control the internal relative humidity to <1% RH, preventing medicine reactions and reducing potency.
- Effervescent tablets (vitamin C, Alka-Seltzer): The COC (cyclic olefin copolymer) blister cavity can effectively block carbon dioxide and prevent pre-foaming. Secondly, the chemical inertness of COC packaging enables it to not react with citric acid/bicarbonate.
- Proton pump inhibitors (omeprazole): Using nitrogen flushing blister packaging technology and high-barrier aluminum-plastic composite materials, the residual oxygen content after testing is controlled at <0.5%, which is significantly better than ordinary blisters. Therefore, it is suitable for pills that are easily degraded in acidic environments.
Photolabile Compounds
Advanced blister materials block specific light wavelengths:
| Drug Category | Light Sensitivity | Blister Solution |
| Nitroglycerin | UV degradation | Amber-colored PVC/Alu |
| Riboflavin | Blue light sensitivity | Opaque white COC |
| Nifedipine | Photochemical reaction | Alu/Alu full barrier |
High-Potency and Controlled-Release Medications
- Opioids (Oxycodone ER): Tamper-evident blisters with anti-counterfeiting print
- Oncology Drugs (Capecitabine): Child-resistant push-through designs
- Hormone Therapies (Levonorgestrel): Calendarized blister strips for cycle tracking
Compliance-Critical Regimens
WHO studies show blister packaging improves adherence by 18-25% for:
- Antiretroviral Therapy (ART)
- Tuberculosis Treatment (DOTS programs)
- Oral Contraceptives (21/7 day visual tracking)
Although there’s often seeing some people complain about blister packaging in daily life and on forums, for example, they think such packaging is annoying. But from the perspective of pill packaging, blister packaging not only functioning protection, quantitative supplementation, and tampering prevention, but in fact, for pill takers who may lack extreme professional knowledge, accuracy and convenience are also the advantages of blister packaging, and the dosage is limited and safe.
Blisters vs. Bottles vs. Pouches

In pharmaceutical packaging, the selection between blister packs, bottles, and pouches represents a critical decision that impacts product stability, patient compliance, and manufacturing efficiency. Each format offers distinct advantages tailored to specific drug characteristics and market requirements.
Material Science Perspectives
Blister Films – sophisticated multilayered materials composed of thermoformable polymers laminated with barrier foils – have revolutionized unit-dose packaging through their exceptional protective properties:
- PVC: Standard option (50-100μm), oxygen transmission rate 5-10 cc/m²/day
- PCTFE (Aclar): Ultra-high barrier (<0.01 g/m²/day WVTR)
- COC: Clarity + chemical resistance for biologics
Comparative Performance Data:
| Parameter | Blister (Alu/PVC) | HDPE Bottle | Stand-up Pouch |
| Moisture Protection | 0.1g/m²/day | 0.4g/m²/day | 1.2g/m²/day |
| Oxygen Barrier | <0.5 cc/m²/day | 50 cc/m²/day | 300 cc/m²/day |
| Dose Accuracy | ±0.5% | ±15% | ±10% |
| Packaging Waste | 8g/10 doses | 25g/10 doses | 5g/10 doses |
| Pros | Waterproof, light-shielded, tamper-proofprevents overdose/missed dosesEasy to use for elderly patientsEasy for tracking complianceLess packaging wast | Cost-effective bulk packagingVersatility of pill types applicationsuitable for large-dose shipping | Lowest unit material costCustomizable printing on packagesAdaptable for most pill typesLighter shipping weight |
| Cons | Higher material costLimited flexibility of repackage and for liquids/powdersComplex manufacturing processes | Poor barrier propertiesInaccurate dose meteringTampering riskNot environmentally friendly | poor physical protectionPoor light/oxygen barrierNot acceptable for high-value prescription medicine |
Regulatory Compliance
In the ever-changing regulatory environment, pharmaceutical packaging must balance traditional compliance requirements with emerging sustainability requirements. Today, the choice between blister packs, bottles and pouches affects not only product protection and patient safety, but also environmental compliance and digital traceability.
Blister Packs
Blister packaging maintains regulatory leadership with inherent tamper evidence and superior serialization capabilities. Its unit-dose design excels in compliance tracking while meeting updated child-resistance standards. Recent sustainability mandates are driving material innovations in recycling and PFAS-free components.
Bottles
Bottle packaging faces growing compliance complexity, particularly around serialization durability and EPR requirements. While still viable for bulk generics, new material restrictions and microplastic testing are increasing implementation costs.
Pouches
Pouch packaging benefits from flexible serialization options but struggles with material compliance. Emerging as a sustainable alternative, it requires careful design to meet updated tamper-evidence and dosing integrity standards.
Key regulations are:
- FDA 21 CFR 211.132 (Tamper evidence)
- DSCSA 2025 (Digital tracing)
- TPCH 2025 (Material restrictions)
- USP <661.2> (Microplastic testing)
- ASTM D3475-2025 (Child resistance)
- EMA 2025 Guidance (Dosing integrity)
- State EPR Laws (Recycling mandates)
| Requirement | Blister | Bottle | Pouch | 2025 Change |
| Tamper Evidence | ★★★★★ | ★★★☆ | ★★☆ | +PFAS ban |
| Digital Tracing | ★★★★★ | ★★★★ | ★★★☆ | +NFC option |
| Child Resistance | ★★★★☆ | ★★★☆ | ★★☆ | +Dual-mode |
| Recyclability | ★★★☆ | ★★☆☆ | ★★★★☆ | +EPR fees |
| Global Acceptance | ★★★★★ | ★★★★☆ | ★★★☆ | +PPWR harmonization |
What Are the Functions of Blister Packing Machine?
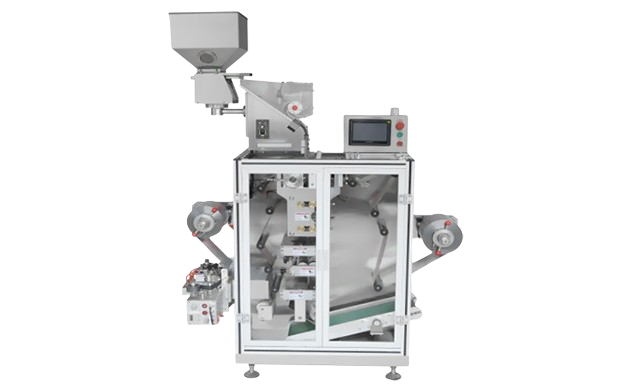
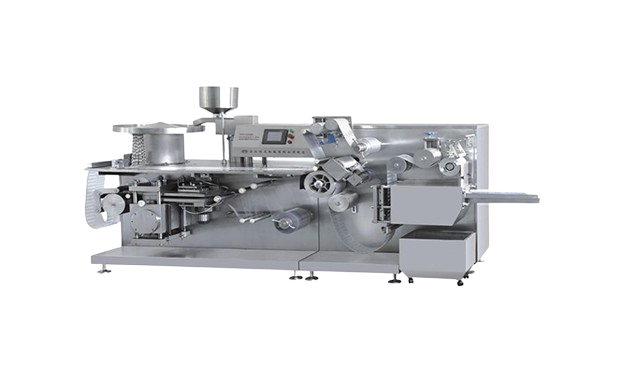
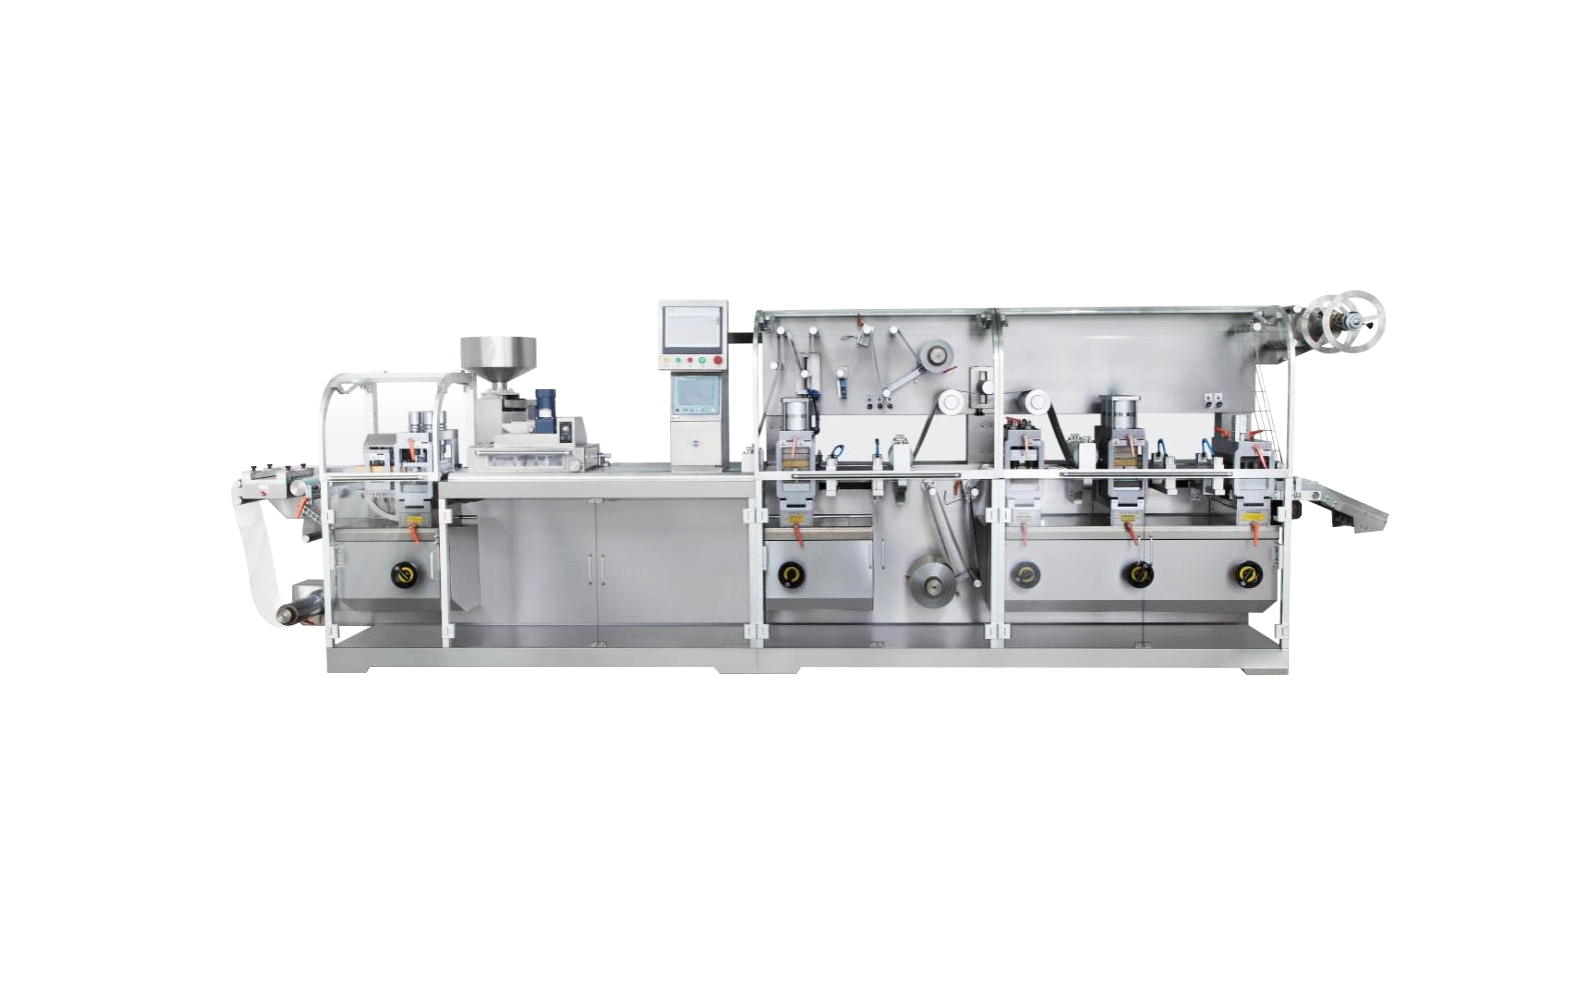
A blister packaging machine is highly specialized pharmaceutical packaging systems designed to automate the production of unit-dose blister packs. These machines play a vital role in ensuring pharmaceutical safety, compliance, and production efficiency. The following details their core features, technological advances, and operational considerations.

Thermoforming
Thermoforming is the first critical stage where the plastic film is heated to a precise temperature and molded into the cavity using a forming die. This process ensures consistent cavity depth and shape to securely hold the tablet or capsule. The blister machine uses servo-controlled heating zones to maintain material integrity while optimizing energy efficiency.
Product Feeding & Inspection
The tablets or capsules are precisely fed into the formed mold cavity using a vibrating feeder. A high-resolution visual inspection system simultaneously verifies correct placement, detects missing or damaged units, and verifies tablet imprints. A reject device automatically rejects defective products, ensuring that only defect-free blisters continue to be produced.
Sealing
The lidding material is heat sealed to the blister film under controlled temperature and pressure. For heat sensitive medications, cold sealing is an option. The closure must be airtight to prevent moisture/oxygen penetration while providing easy access for the patient.
Perforation & Cutting
The continuous blister sheet is cut mechanically or laser cut into individual strips or cells. Perforation lines are added where needed to facilitate opening by the patient. Modern systems achieve clean, burr-free edges even in complex multi-cavity designs while maintaining a positioning accuracy of ±0.5 mm.
Printing & Coding
Each blister is printed with vital information such as batch number, expiration date and barcode via inkjet or laser printing technology. Advanced production lines integrate serial numbering to ensure regulatory compliance. The printing process must maintain >99.98% readability at production speeds of up to 600 blisters/min.
Top Blister Packing Machine Manufacturers
SED Pharma

Website: https://sedpharma.com/
Core products: Pharmaceutical Blister Packaging Machine
Description:
SED Pharma is deeply involved in the pharmaceutical industry and is committed to bringing unlimited possibilities to pharmaceutical packaging. The blister packaging equipment we developed can be regarded as an irreplaceable influence in the industry, both in terms of delicate processes and continuous operations. In order to meet the needs of users, we conduct in-depth testing and research on various dosage forms, packaging materials, and packaging speeds, etc. And no worries about the compliance of drug packaging, as we have obtained relevant certifications.
IMA Group

Website: https://ima.it/
Core products: Blister Pack Machine for Pharmacy
Description:
IMA Group develops photo packaging technology for stand-alone or integrated solutions, with a focus on sustainable blister packaging materials. Fifty years of technical experience have created new performance and efficiency values for their equipment, including flexible use of equipment to open up more possibilities for processing blister packaging. As one of their superhuman advantages, they have customizable packaging solutions.
Mediseal

Website: https://www.koerber-pharma.com/
Core products: Pharma Blister Pack Equipment
Description:
Mediseal‘s blister packaging system is extremely diverse, with a wide range of products, from tablets to medical products, all of which can meet packaging needs. Designed to shorten production time, provide flexible solutions and meet the highest quality, it is the cornerstone of pharmaceutical manufacturers’ production capabilities. Mediseal’s blister packaging machine adopts a modular design, with clear divisions of each area, and all equipment is equipped with a transparent cover to ensure that the packaging process is transparent and meets hygiene standards.
Uhlmann Group

Website: https://www.uhlmann.de/
Core products: Pharmaceutical Blister Packer
Description:
Uhlmann has a range of high-quality blister packaging machines with packaging speeds ranging from 200 to 1300 packs/min for a wide range of solid and parenteral products. Uhlmann offers a unique combination of performance, quality and efficiency. Its solutions enable GMP-compliant blisters of capsules, dragees and tablets with the same reliability as vials, ampoules and syringes.
If you are happen to do research on companies of blister packaging machines who are in top ranks, read this article to better compare:
Conclusion
Blister packs have evolved from a simple protective shell to an advanced drug delivery platform that integrates material science, Industry 4.0 automation and patient-centric design. While vials remain cost-effective for generic drugs and pouches dominate the powder market, blister packaging offers unmatched performance for sensitive, high-value drugs that are critical to adherence.
Maybe the blister pack of 2030 could be both a container and a “drug delivery device” – making investment decisions today critical to long-term competitiveness.